Inconel 718 Machining — Work-Hardening Under Control, in Batch Production

Nickel superalloy parts held to 0.005 mm and Ra 0.4 μm — 5-axis on Mazak VARIAXIS centers, five-face gantry to 6 m, deep holes production-proven to 10,000 mm. Inconel 718 runs on our floor every week, not once a year. Upload your drawing via the RFQ form — an engineer replies within 24 hours.

Attach your drawing (STEP / DWG / DXF / PDF) and the material spec. NDA welcome — yours or ours. Within 24 hours an engineer — not a salesperson — responds with manufacturability feedback.
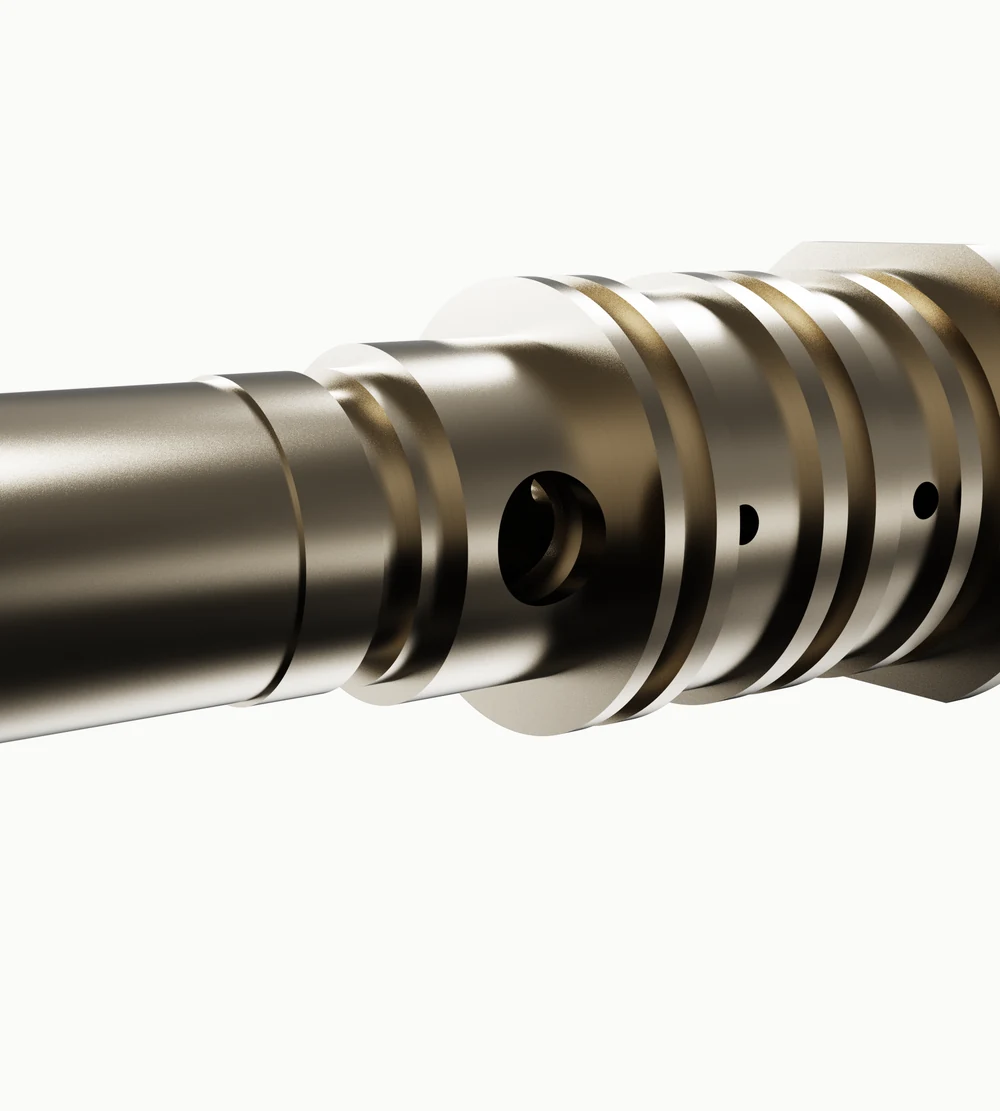
Nickel superalloy part on a white background — machined faces catching the light
Nickel superalloyInconel 718Weekly production, not an annual event

Why Inconel 718 Is Hard to Machine

Inconel 718 is a precipitation-hardened nickel superalloy that keeps its strength where most steels have already given up — which is exactly why your part is made from it, and exactly why many shops fail at it.

The failure mechanism is work-hardening. The austenitic nickel matrix hardens the instant it is deformed. Cut it with a dull tool or a timid feed and the edge rubs instead of shears; the surface layer hardens mid-cut, pass after pass, until the tool is machining something far harder than the bar that arrived. Add two more traits — thermal conductivity so low that cutting heat concentrates in the tool edge instead of the chip, and hard abrasive carbide particles in the matrix — and you have an alloy that punishes hesitation and rewards decisive, rigid, well-cooled cuts.

Every one of these behaviors is learned in scrapped parts and worn tooling, over years. We have already paid that tuition.

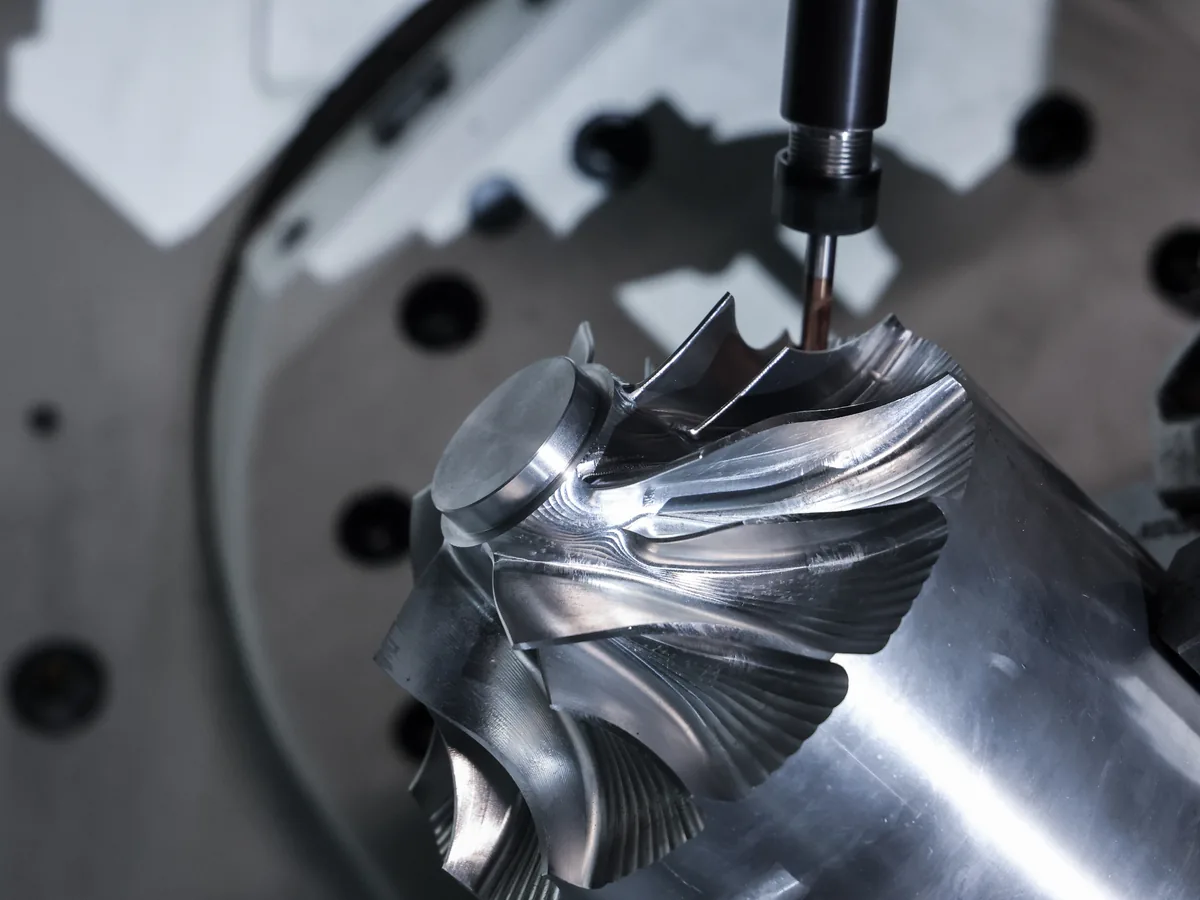
Five-axis milling of an integral impeller in a nickel-base alloy
Cutting the family that fights back — 5-axis, in nickel-base alloy

Capability — Inconel 718 × Our Processes

ProcessEnvelope / range in Inconel 718Notes
5-axis CNC machiningMazak VARIAXIS i-800 (Ø800 class) & C-600 (Ø630 class); meter-to-12 m parts on self-built FWG-M1260 five-face gantry (travels 6/8/12 m)True simultaneous 5-axis; A-axis 360° / B-axis ±120°; in-house CAM
CNC turning & mill-turnTurning to Ø800 × 8,000 mm (FWT-80800); shop envelope Ø1,000 × 10,000 mm; mill-turn in one clamping (Mazak INTEGREX i-500S / i-400S)±0.01 mm at the machine; slender shafts to 4,500 mm as routine
Deep-hole drilling (BTA)Ø20–360 mm; machine envelope 12,000 mm; production-proven Ø20–300 × 10,000 mmStraightness 0.5 mm/m; eccentric bores, multi-step seal bores in one setup
Gun drillingØ2–40 mm, depths to 6,000 mm; hole tolerance ±0.02 mm, bore finish Ra 1.6 μm13 machines, all designed and built in-house
Precision grindingCylindrical to φ500 × 3,000 mm (MQ1350B), φ125 × 500 mm (MGB1412); internal φ200 × 250 mm (×2, Swedish); to 0.005 mm & Ra 0.4 μmInconel ground as routine
Welding & hardfacingTIG and laser welding of Inconel 718; narrow-gap welding of superalloys to 60 mm depthIn-house, no subcontracting
Heat treatment & surfaceVacuum hardening, stress-relief, hard chrome / electroless nickel / PTFE coatingCoating allowance engineered into the machining program

Where We Run It

Commercial aviation — a national civil aircraft program. Semi-finish and precision machining of nickel-superalloy structural parts, on Mazak VARIAXIS 5-axis centers and our self-built FWG-M1260 five-face gantry, with final operations completed by a certified member of our group. In production today:

Air ducts →Seal-ring shields →Valve mounting seats →

We support commercial aviation programs only.

Oil & gas drilling. Inconel 718 MWD & LWD housings → in production for offshore downhole tools rated at 180 °C / 180 MPa, proven in sustained field operation.

Incoloy 925 — the companion grade on this page — runs as high-strength, corrosion-resistant shafts and housings for oilfield service, machined with the same superalloy discipline.

Machined structural part on a white background
Structural part — nickel superalloy
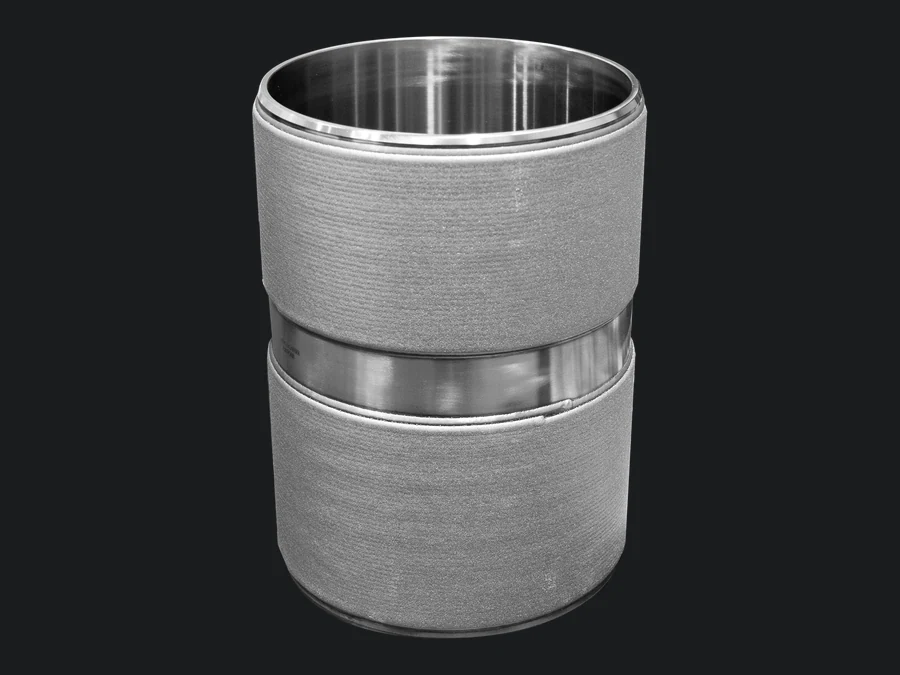
Drill collar section — wear band and wall thickness visible
Drill collar — wear band and bore

Machining Strategy

We do not publish speeds and feeds — those are earned per part, per feature, and frozen into the routing once proven. What we can tell you is the doctrine:

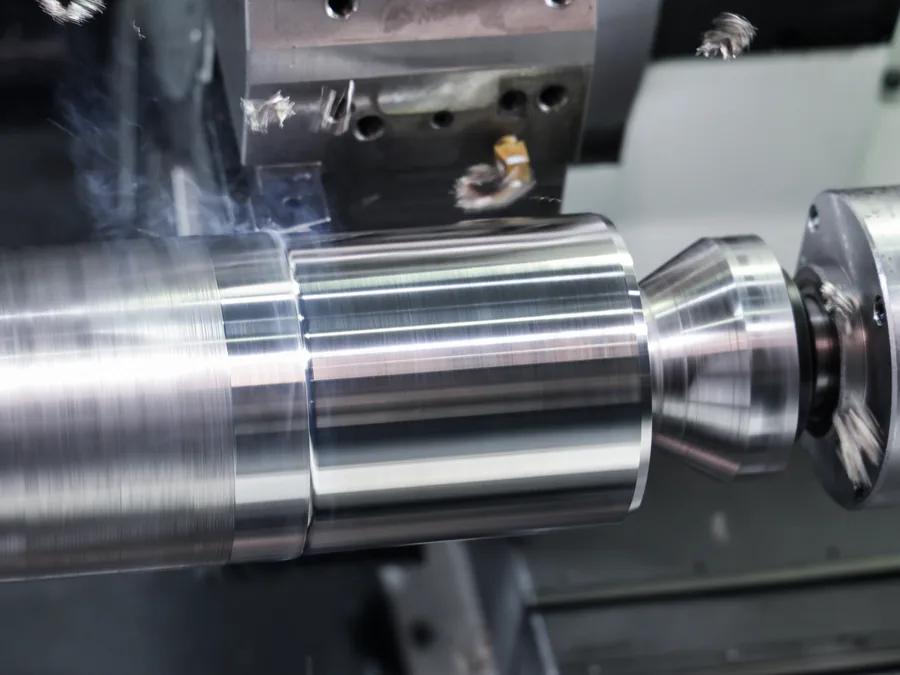
Ceramic tool turning — heavy stock removal, chips flying
Ceramic tool, roughing — stock removal before the finishing passes

Traceability & Verification

Difficult alloys demand proof at both ends — what the mill delivered, and what we shipped:

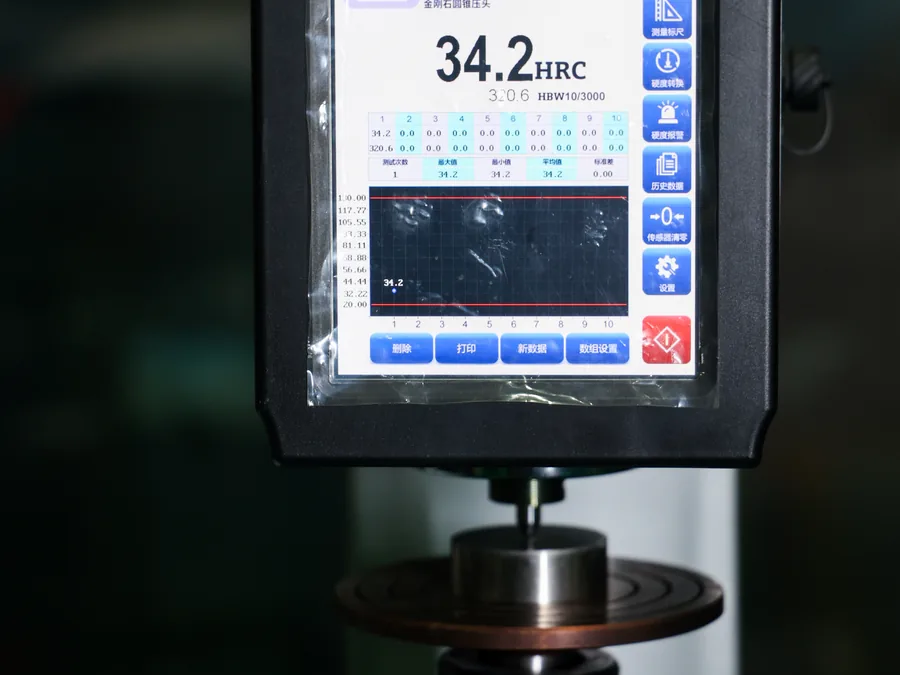
Hardness and composition data being verified in the lab
Chemistry and hardness, checked before the first cut

FAQ

Q: Can you machine Inconel 718 in the aged (precipitation-hardened) condition?

Yes — and we plan for it. Where the print requires it, roughing is sequenced around heat treatment so finishing stock remains after aging, and final dimensions are closed by grinding. Tell us the specified condition and we will propose the routing.

Q: What part sizes can you handle in Inconel 718?

From small seal-ring guards to meter-class 5-axis parts on Mazak VARIAXIS centers and 12 m five-face gantry work, turned parts to Ø800 × 8,000 mm, and deep bores production-proven to 10,000 mm. Single prototypes through batch production — from 1 piece, no minimum order.

Q: Do you also machine Incoloy 925?

Yes. Incoloy 925 runs in production as high-strength, corrosion-resistant shafts and housings for oilfield service, with the same traceability and inspection discipline as 718.

Q: Do you support aviation work?

We support commercial aviation programs only — semi-finish and precision machining of nickel-superalloy structural parts for a national civil aircraft program, with final operations completed by a certified member of our group.

Q: How do you verify the material is really 718?

Every incoming lot is verified by optical emission spectrometry before it enters production, chemistry and mechanical properties are checked in-house, and the mill heat number follows your part to the inspection report. Certificates ship with every order.

See all questions we get asked →

Send the 718 Part That Keeps Failing Elsewhere

Upload your drawing with the alloy condition — aged, annealed, or as-rolled. Within 24 hours, an engineer who runs these alloys weekly responds with a routing and a date.

Related: Materials Hub|Aerospace|Oil & Gas|5-Axis Machining

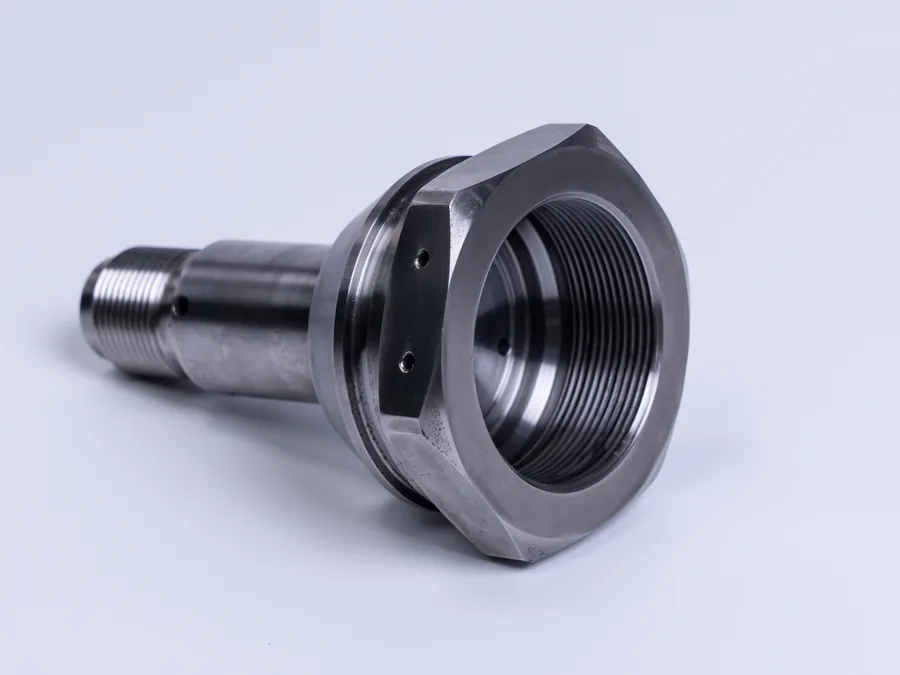
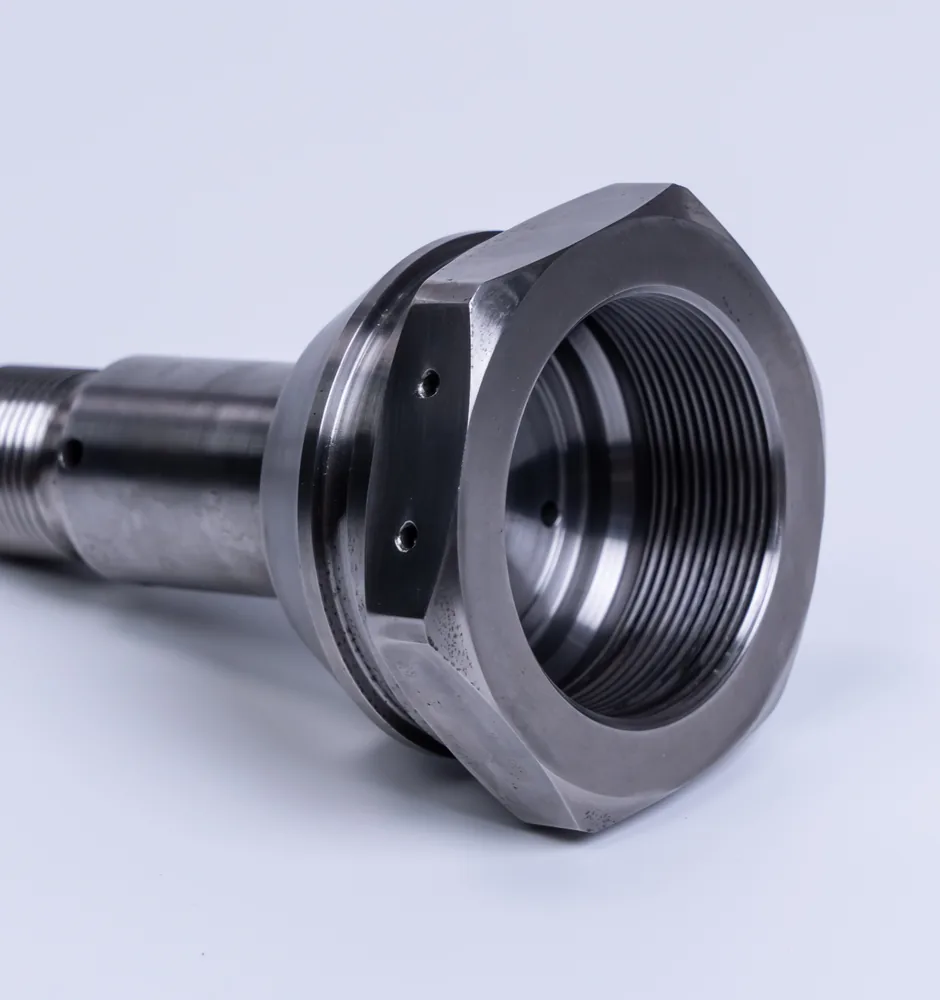
Safety valve — large internal thread and hex flange
Safety valve

Trademark notice: INCONEL and INCOLOY are registered trademarks of Special Metals Corporation (PCC). They are used on this page solely to describe the alloys we machine (UNS N07718 / N09925); no affiliation or endorsement is implied.