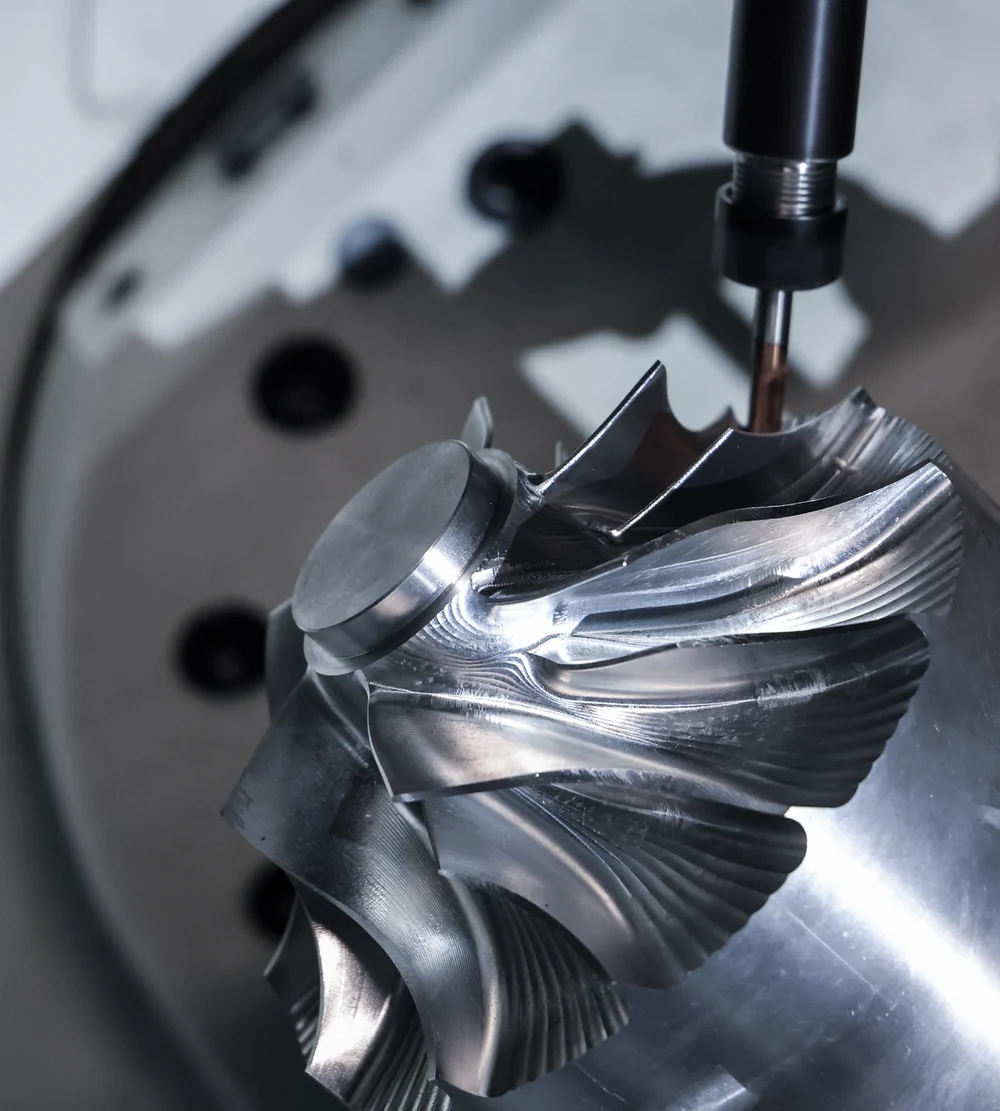
Five-axis machining is common. Five-axis machining at six meters, in Inconel, is not.
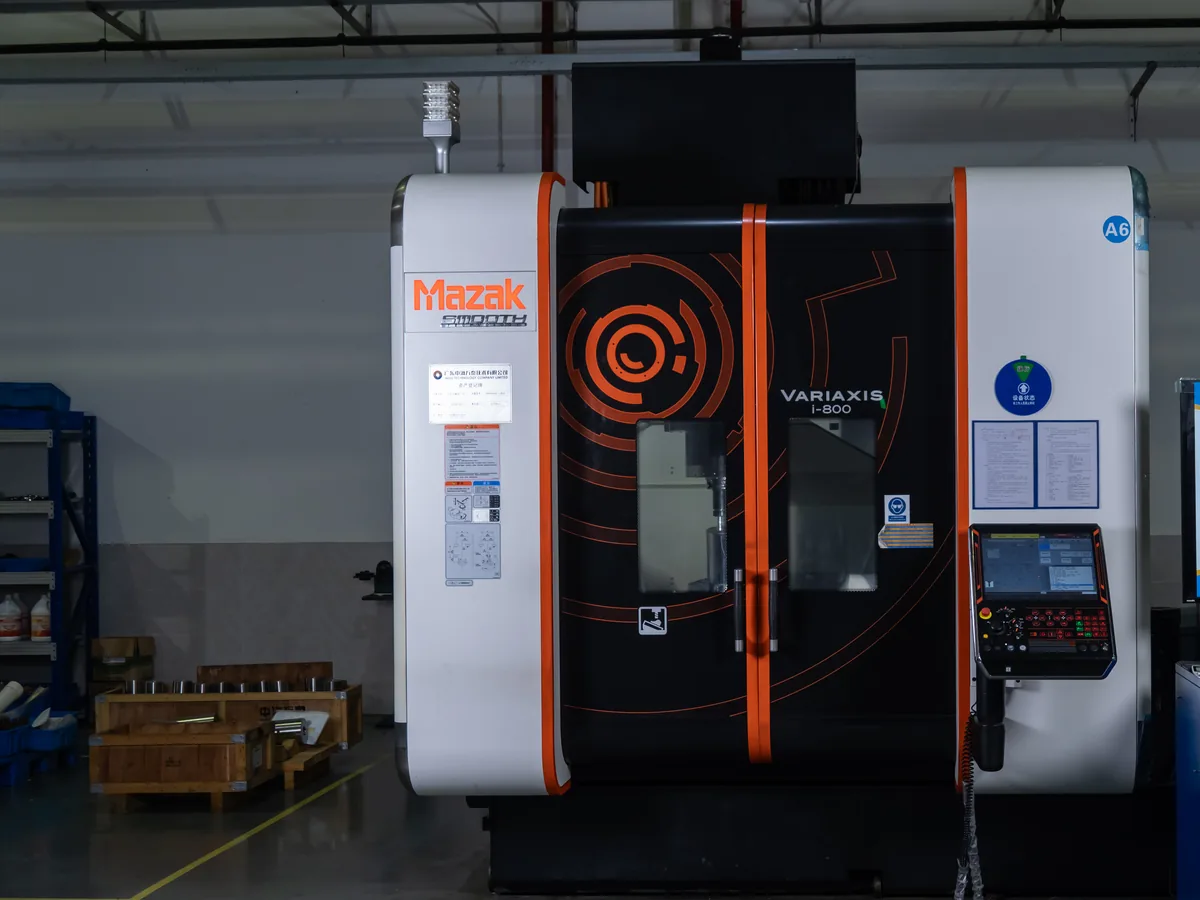
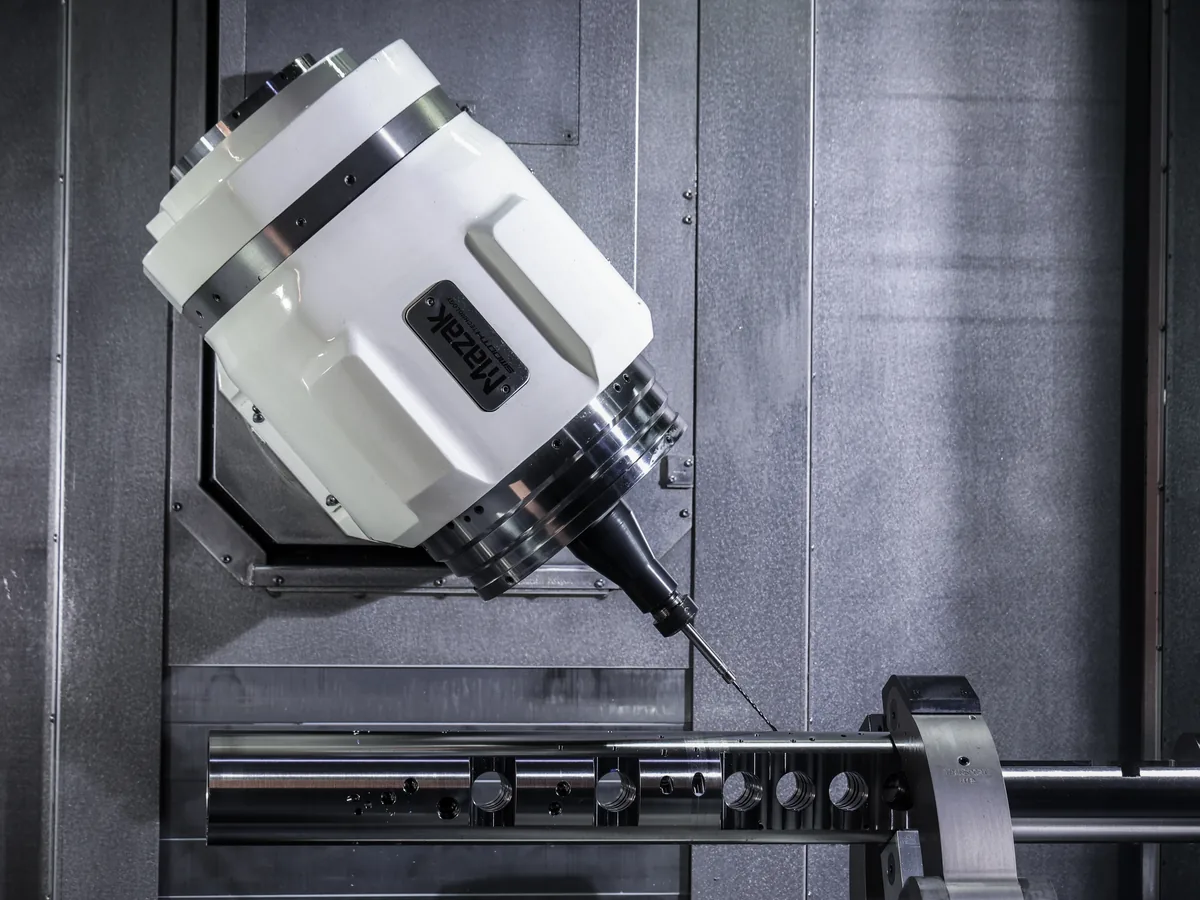
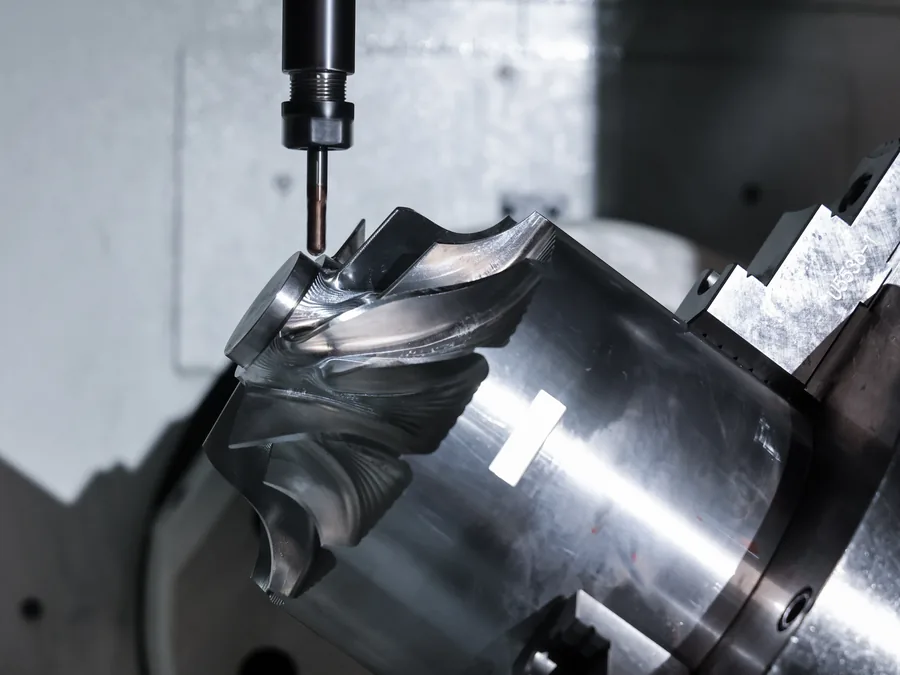
Simultaneous 5-axis machining on imported Mazak VARIAXIS centers to φ800 mm class — and long-axis parts to Φ400 × 6,000 mm on our self-built FWV-M6080 5-axis drilling-boring center — complex contours and structural parts in superalloys and titanium, held to ±0.01 mm at the machining center. The line-up includes machining centers we designed and built ourselves.

Every time a part is re-clamped, accuracy leaks. Five-axis machining exists to remove the clamps:
Complex parts finished in a single clamping: no accumulated fixture error, no datum shifts between operations, no queues between machines
Holes, pockets, and contours on five sides stay in true position to each other, because the part never leaves its first setup
The head tilts to the feature, so shorter, stiffer tools reach the geometry: less deflection, less chatter, better finish
At meter scale, thermal growth and structural rigidity dominate. A degree of spindle warm-up becomes microns at the tool tip, meters away. Large-format 5-axis is a different discipline from small-part 5-axis — and it is the one we practice
Inconel and titanium multiply cutting forces and punish every weakness in the chain: machine rigidity, toolholding, CAM strategy, coolant. Simultaneous 5-axis in superalloys is where equipment and experience are audited together
| Parameter | Capability |
|---|---|
| Working envelope | Simultaneous 5-axis to φ800 mm class — imported Mazak VARIAXIS i-800 (φ800/850 mm) and VARIAXIS C-600 (Φ630/650 mm); long-axis parts to Φ400 × 6,000 mm on our self-built FWV-M6080 5-axis drilling-boring center |
| Rotary axes | A-axis 360° / B-axis ±120° |
| Spindle | 26 kW, 12,000 rpm, HSK63 |
| Tolerance | ±0.01 mm at the machining center |
| Surface finish | To Ra 0.1 μm (with in-house grinding) |
| Materials | Inconel 718, Incoloy 925, titanium TC4/TC11/TC18, high-strength steels, P550 |
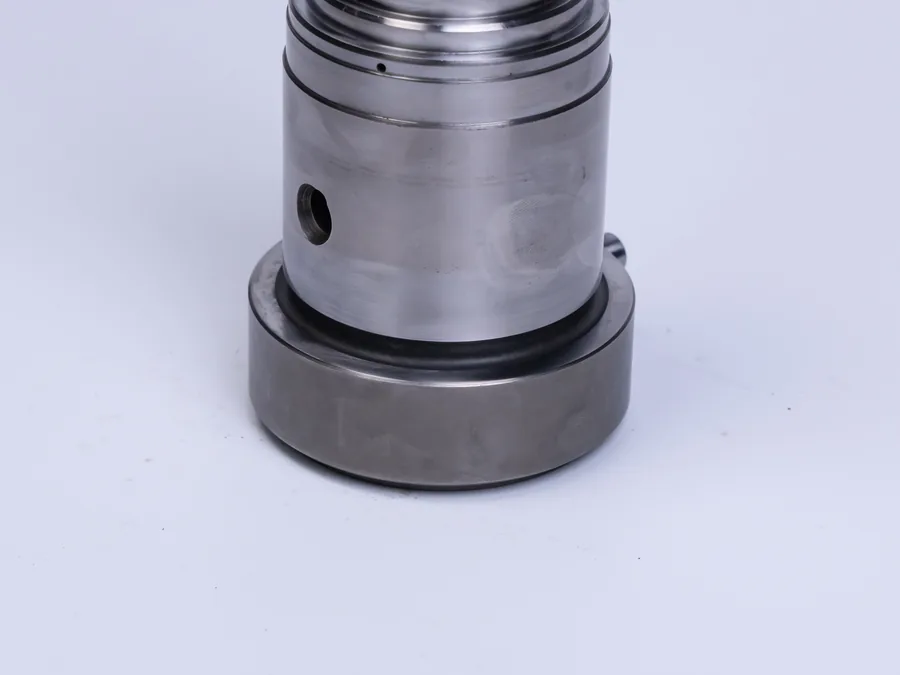
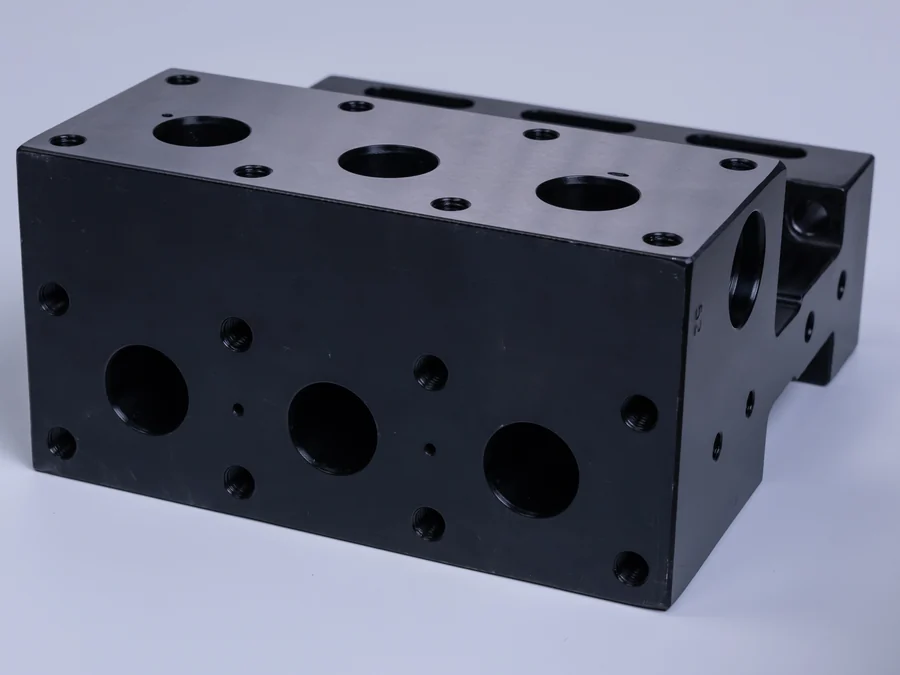
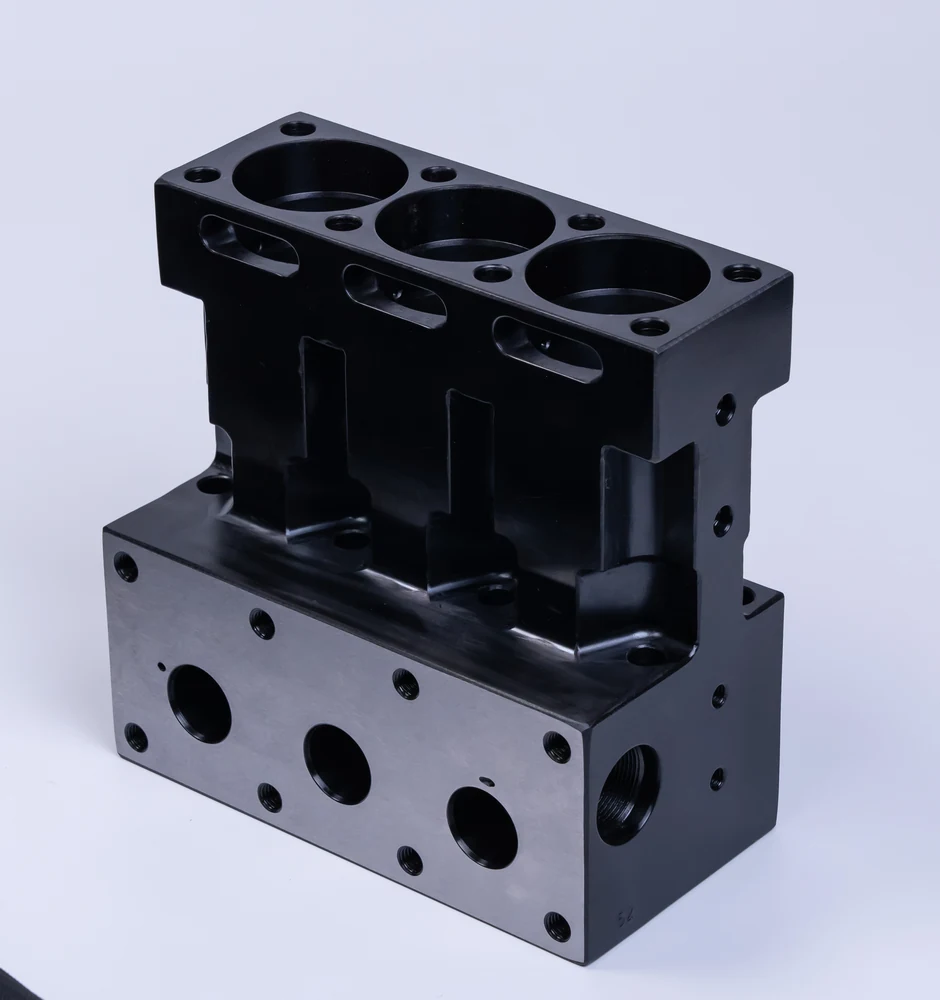
| Typical parts | Structural housings, large housings, complex-contour parts, control valve bodies |
| Equipment note | Two imported Mazak VARIAXIS centers plus the FWV-M6080 — designed and built in-house, Siemens control |


Most five-axis suppliers only buy their machines. We also build them.
Our FWV-M6080 five-axis drilling-boring center — Φ400 × 6,000 mm — was designed and built in-house: travels, structure, and rigidity specified backward from the parts that needed them. That origin shows up where it matters: when a meter-scale structural part in titanium starts to fight the program, the people adjusting the process understand the machine’s stiffness envelope and thermal behavior from the inside — because they are the ones who designed it.
Large-format five-axis is also a systems problem: fixturing for meter-scale parts, process discipline over hour-long cuts, thermal management across the full travel. We solve these daily, on our own equipment, for parts where failure is not an option.

| Industry | 5-axis application | The record |
|---|---|---|
| Aerospace | Structural parts & housings in nickel-base superalloys | Qualified supplier in a national civil aircraft program — precision semi-finishing |
| Oil & Gas | Downhole tool housings & structural parts | Manufacturing partner of a rotary-steerable drilling program in China |
| Robotics | Joint housings, manipulator structural parts | Deep-sea manipulator parts in production |


Simultaneous 5-axis — our machines run true five-axis simultaneous work, down to cross-holes at any angle. Tell us the part and we will tell you which strategy it needs.
Simultaneous 5-axis work goes to φ800 mm class on our imported Mazak VARIAXIS machining centers; long-axis parts — to Φ400 × 6,000 mm — are machined in one setup on our self-built FWV-M6080 5-axis drilling-boring center.
Tolerance depends on feature size, geometry, and material — on large parts especially. Send the drawing; we will state what we can hold, feature by feature.
Yes — single pieces and small batches run through our Custom Manufacturing → line; batch programs run on the production floor.
In-house — simultaneous 5-axis toolpaths are programmed by our own process engineers, side by side with the people who run (and built) the machines.
Upload your drawing — structural housing, large housing, or complex contour. Within 24 hours, an engineer responds with manufacturability feedback.
Related: Capabilities Hub|Aerospace|Precision Grinding