EDM Machining Services

A cutting tool needs somewhere to go. A spark does not.

Sinker EDM to ±0.01 mm, wire EDM to ±0.002 mm, deep-hole EDM to 800 mm — in-house, on machines we designed and built. For internal cavities, curved flow channels and cross-holes no cutter can reach.

Send the drawing — mark the features a cutter cannot reach. NDA welcome.
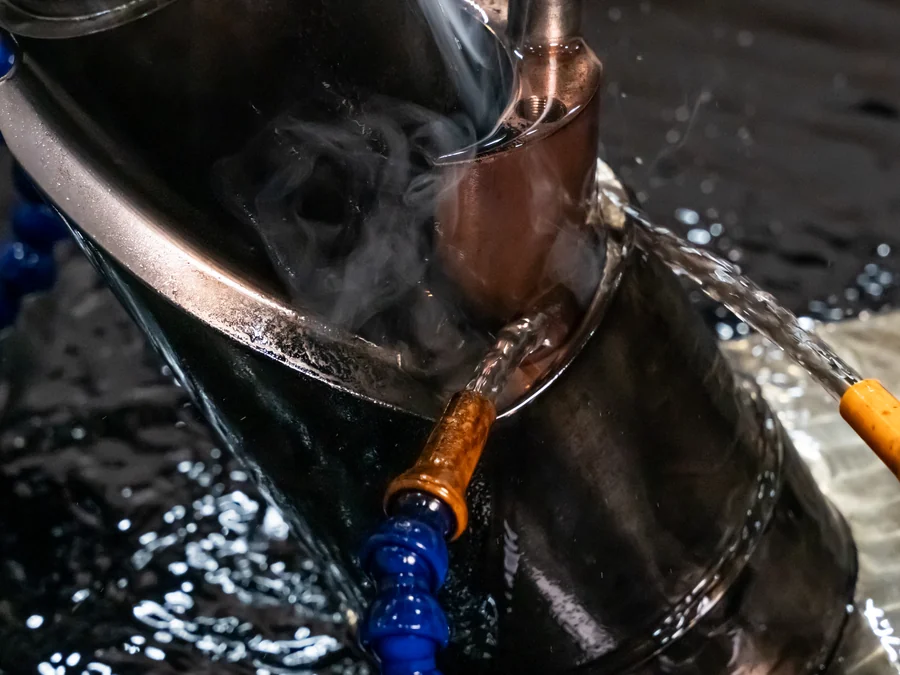
Copper electrode discharging in a deep cavity — dielectric flushing and sparks at the gap
Deep-hole EDMCopper electrodeSpark erosion, dielectric flushing the gap

Why EDM Is the Process of Last Resort

Some geometry has no milling solution. EDM is how it gets made:

That is why we treat it as the process of last resort — not the cheapest or the fastest, but for some geometry the only one that works.

The electrode does not have to spin — it only has to get there

Capability

Four EDM processes, four different jobs:

EDM processTolerance & finishWhat it is for
Sinker EDM (die-sinking)±0.01 mm · Ra 0.8 μmInternal cavities, deep slots and sharp internal corners in hardened material
Wire EDM — fine±0.002 mm · Ra 0.4 μmPrecision profiles, punches and dies, parting already-hardened parts
Wire EDM — fast±0.01 mm · Ra 3.2 μmRoughing and non-critical profiles
Deep-hole EDMØ ±0.01 mm · Ra 0.8 μmComplex cavities and internal features to 800 mm deep — on a machine we designed and built

Equipment — Including a Deep-Hole EDM We Built Ourselves

Sinker EDM. Six CNC-800 mirror-finish sinker EDMs on our own floor — the machines behind our mould and die work.

Ram-type mirror EDM. For larger mould and die work, a ram-type mirror-finish machine runs at our joint venture.

Wire EDM. Fine and fast wire machines, held to ±0.002 mm and ±0.01 mm respectively.

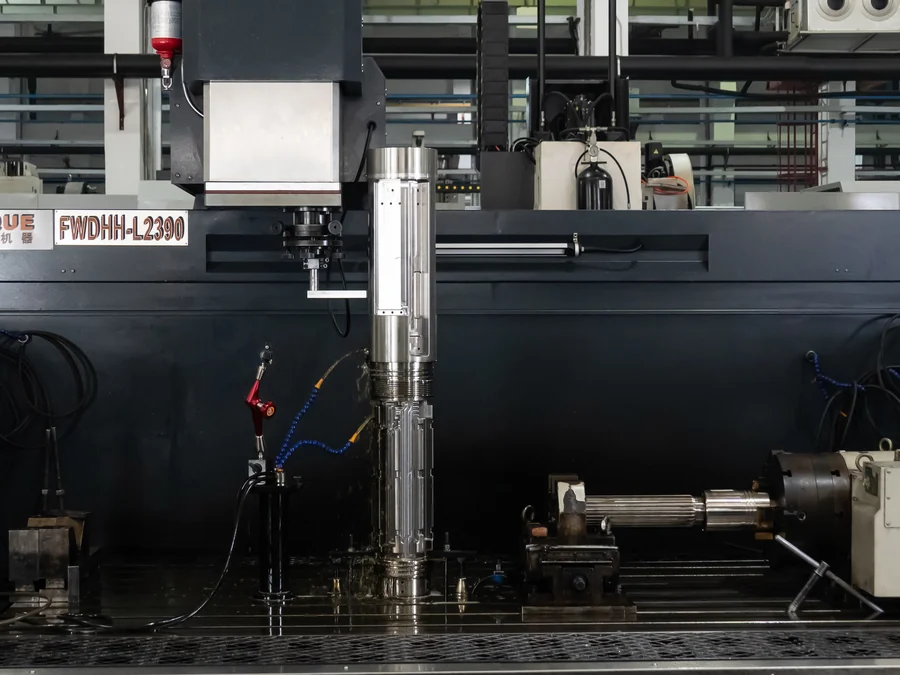
Deep-hole EDM — our own design. Two models, FWDHH-M4080 and FWDHH-L4070: three-axis CNC machines on an integrated gantry frame, three axes simultaneous, tuned for the same difficult alloys our other lines run — Inconel 718, non-magnetic stainless and titanium. They run at our joint venture.

The step that started it. On a hydraulic control unit body — three groups of high-precision deep bores inside one part — the deep-hole EDM operation used to be sent overseas, and the route ran about five months. We built our own deep-hole EDM, working through dielectric sealing and Z-axis accuracy, and brought the operation back in-house. The cycle came down by roughly a third.
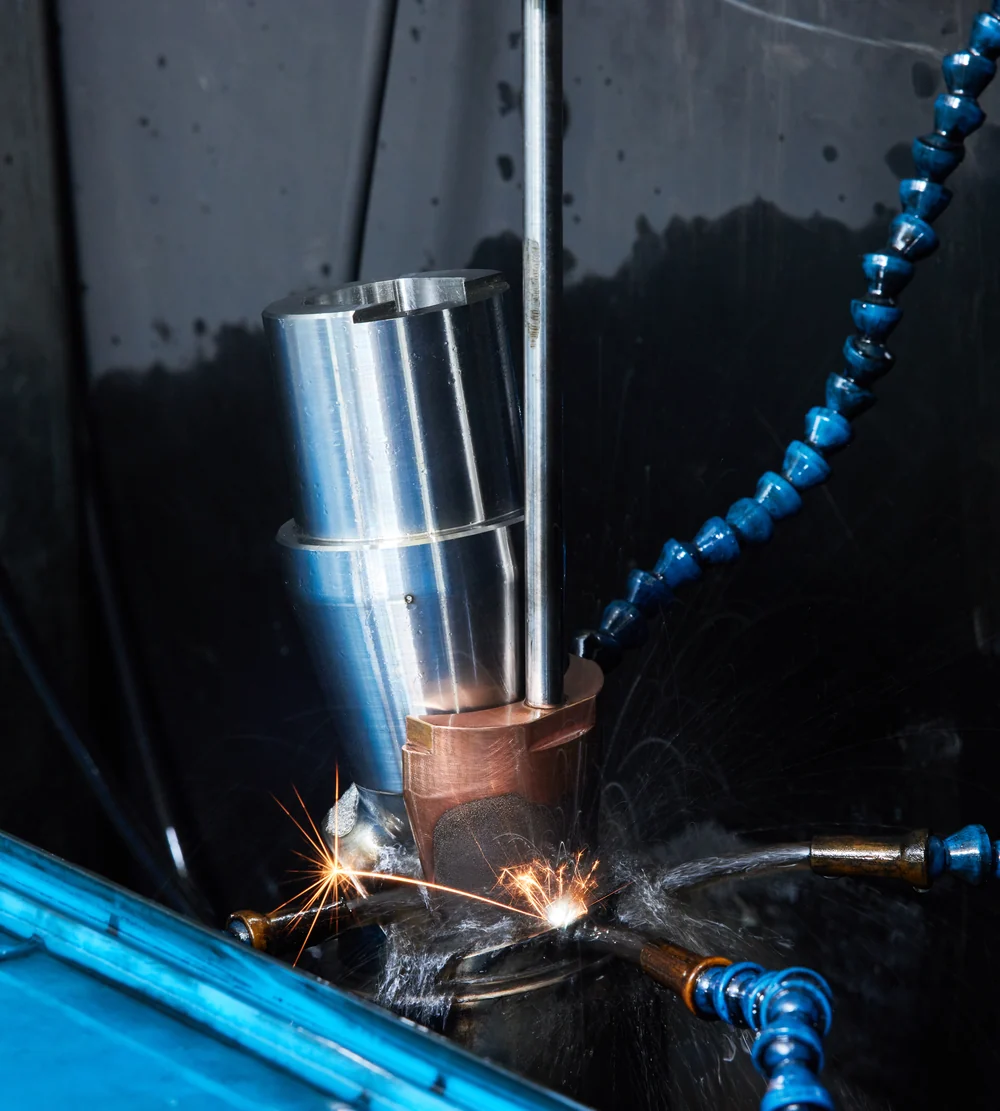
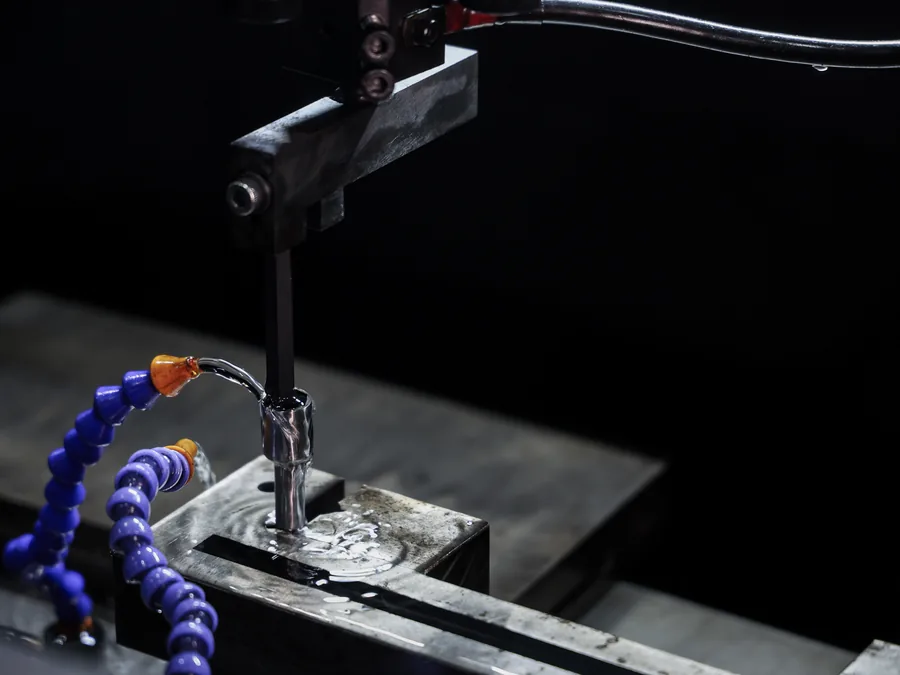
EDM machine head with electrode holder and flushing nozzles over a workpiece
On the floorSix sinker EDMsMirror-finish, mould and die work

Where Our EDM Is Working

ApplicationWhy EDMOur record
Hydraulic control unit bodiesThree groups of high-precision deep bores inside one partDeep-hole EDM brought onto machines of our own design — cycle cut by about a third
Downhole tool housingsInternal cavities and cross-holes no cutter can reachIn production for rotary-steerable and MWD/LWD programs
Moulds & diesSharp internal corners, mirror finishes, hardened steelThe company began as a tooling & mould shop in 1993 — this is where we come from
Hardened & exotic partsHardness-independent removal, no tool wearInconel 718, non-magnetic stainless, titanium — in batch production
FWDHH-L2390 deep-hole EDM — the self-built machine with a long workpiece clamped in position
FWDHH-L2390 — the deep-hole EDM we built, workpiece in position
Copper electrode eroding a hardened part — dielectric flushing the gap
Electrode eroding a hardened part — dielectric flushing the gap

FAQ

Q: What can EDM do that milling cannot?

Reach geometry a rotating cutter physically cannot — internal cavities, curved flow channels, cross-holes and sharp internal corners — and do it in material that is already hardened. No cutting force also means no deflection on slender or thin-walled parts.

Q: How long does EDM take?

A single deep feature can run one to two weeks. EDM is not a shortcut — where a cutter can do the job, we use the cutter, and we quote EDM only where it is the right process.

Q: Can you EDM hardened or exotic material?

Yes — hardness is irrelevant to the process. We run EDM in production on hardened tool steel, Inconel 718, non-magnetic stainless and titanium.

Q: Do you offer wire EDM as well as sinker?

Both. Fine wire to ±0.002 mm with Ra 0.4 μm; fast wire to ±0.01 mm; sinker EDM to ±0.01 mm with Ra 0.8 μm.

Q: Can you EDM customer-supplied parts?

Yes — full service from our material, or your supplied parts

See all questions we get asked →

Send the Geometry No Cutter Can Reach

Upload your drawing with the features a cutter cannot reach — an internal cavity, a curved channel, a cross-hole. Within 24 hours, an engineer responds with process feedback.

Related: Capabilities Hub|Deep-Hole Drilling|Special Processes|Custom Machine Tools

Pump body — threaded port on the machined top face
Pump body