A partnership measured in drilled hole, not in purchase orders.
As manufacturing partner of a rotary-steerable drilling program in China, our components are machined from non-magnetic alloys for service at 180 °C and 180 MPa — and have been in continuous production for years.

A downhole tool is not a part that must work. It is a part that must keep working in a place nobody can reach.
When a downhole part fails, the string is fished, or the hole is lost. The cost is counted in days of rig time, not in parts
The service envelope is hot and it is under enormous pressure. Material choice is not a preference here; it is the design
P550 and 15-15-class nitrogen-strengthened non-magnetic steels work-harden severely. A dull edge does not cut them, it hardens them
The housings and collars are long, thin-walled and full of precision bores. Straightness and wall thickness are process problems over that length
The paper trail is part of the part. Every heat number, every certificate, every examination record

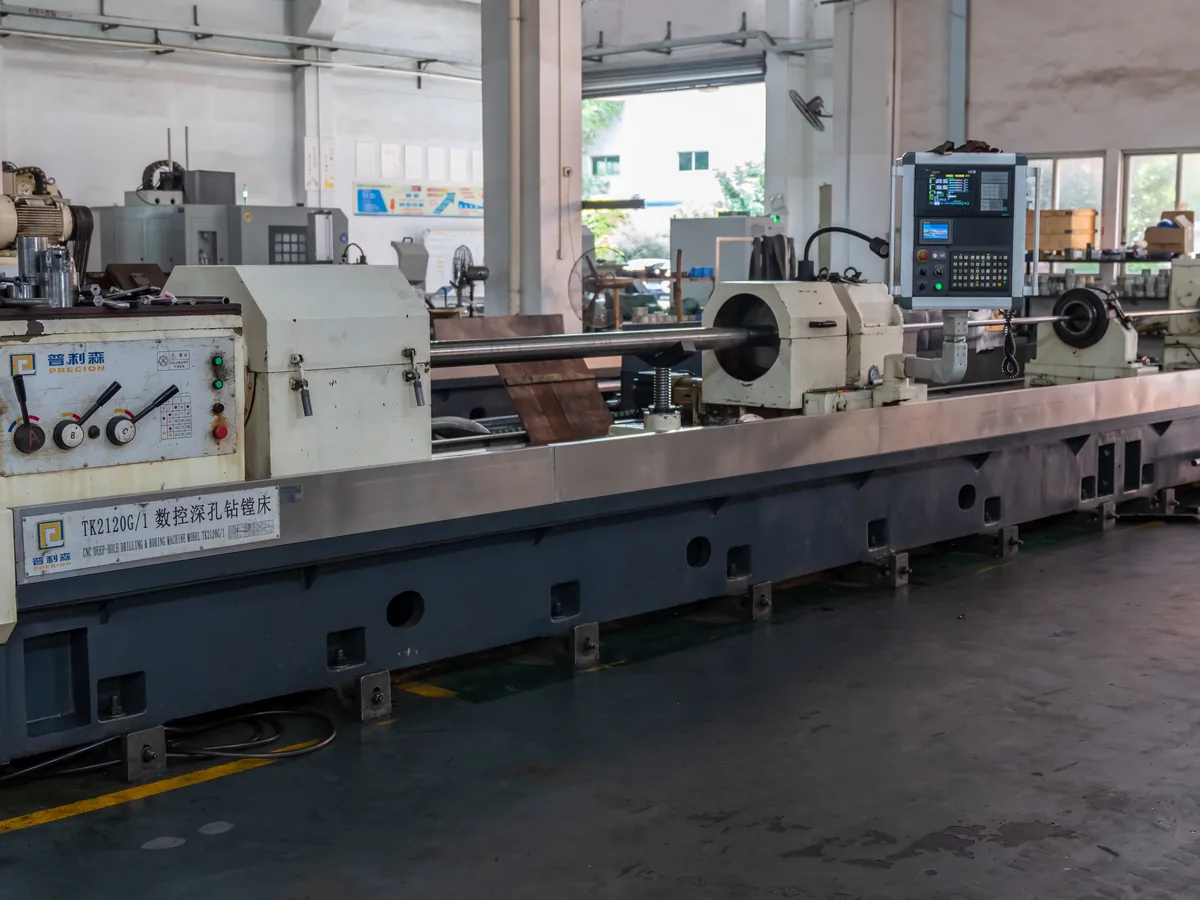
A 7-metre sonic drill collar, with a cross-slot milled 3 metres inside it.
The part itself is a measurement problem before it is a machining problem: how do you establish position three metres deep inside a seven-metre bore, and then hold it while you cut? The answer was not a single machine or a single operation — it was a routing, a fixturing approach and a metrology sequence developed for that one part.
That work supported a full domestic substitution of the component: better detection and recovery efficiency in oil and gas exploration, without waiting on an imported part.


This is a standing manufacturing partnership, not a completed project
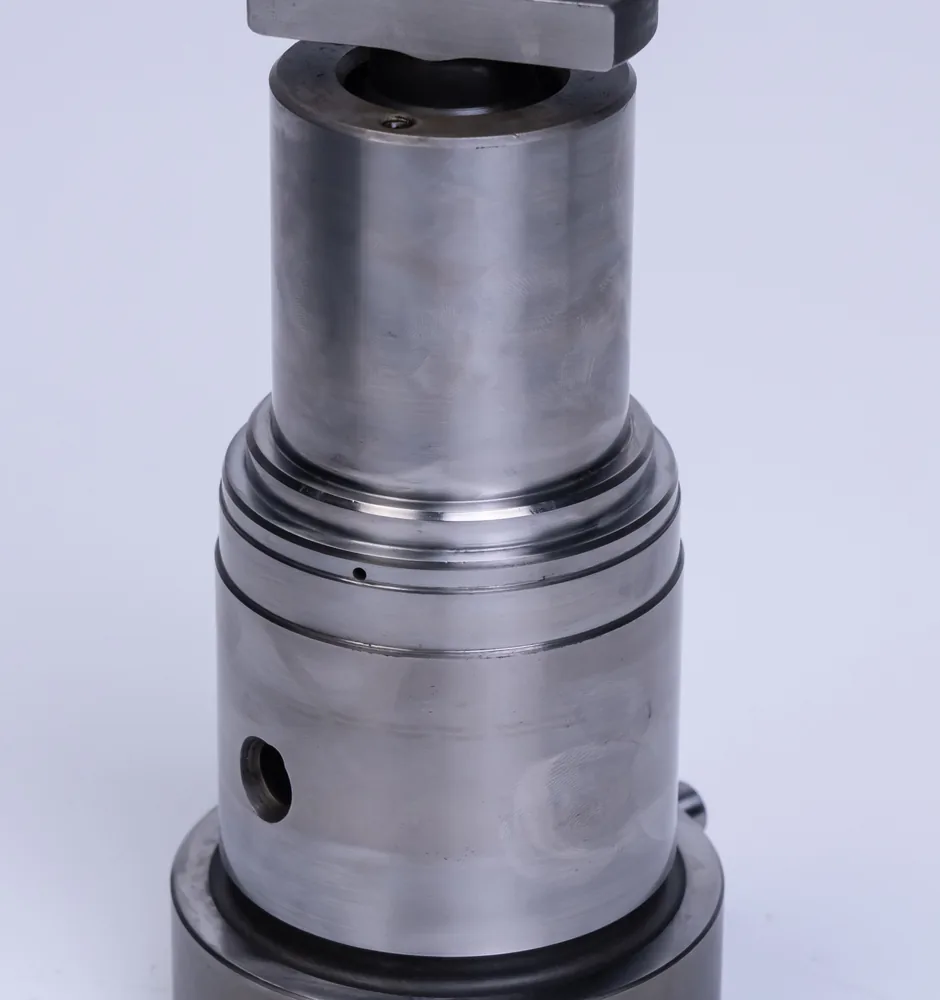
P550 and 15-15-class nitrogen-strengthened non-magnetic steels, in batch, for drill collars across the variant family: sonic, pulser and turbogenerator collars
Push blocks and ribs are in production
NC38, NC46 and NC50 series, to the connection type your drawing calls out
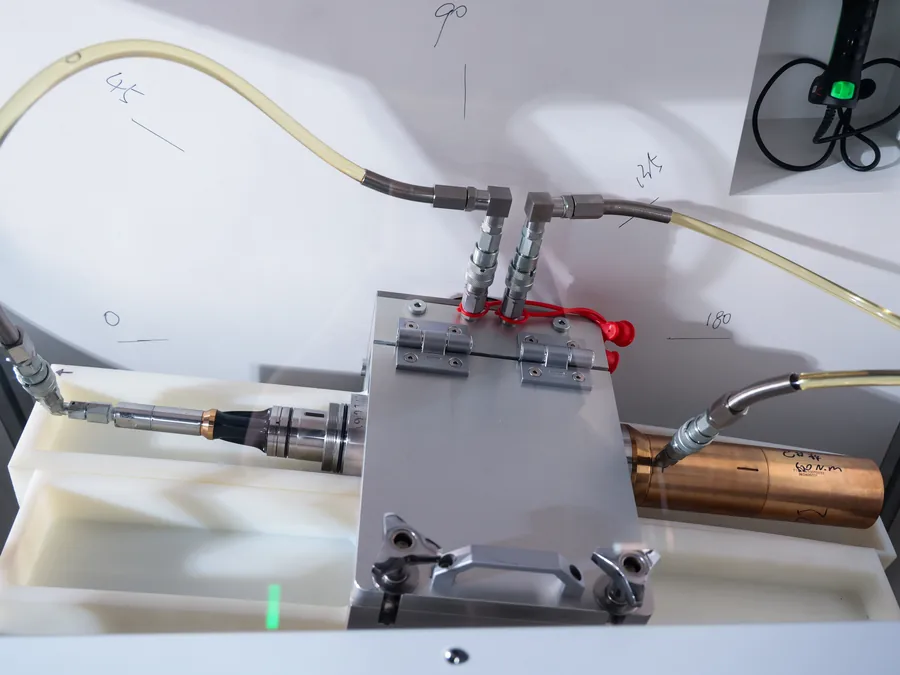
Through our joint venture, parts and the tools they belong to are proven on a high-temperature/high-pressure vessel rated 180 °C / 180 MPa with a Ø450 × 10,000 mm chamber — the facility was built to reproduce the well
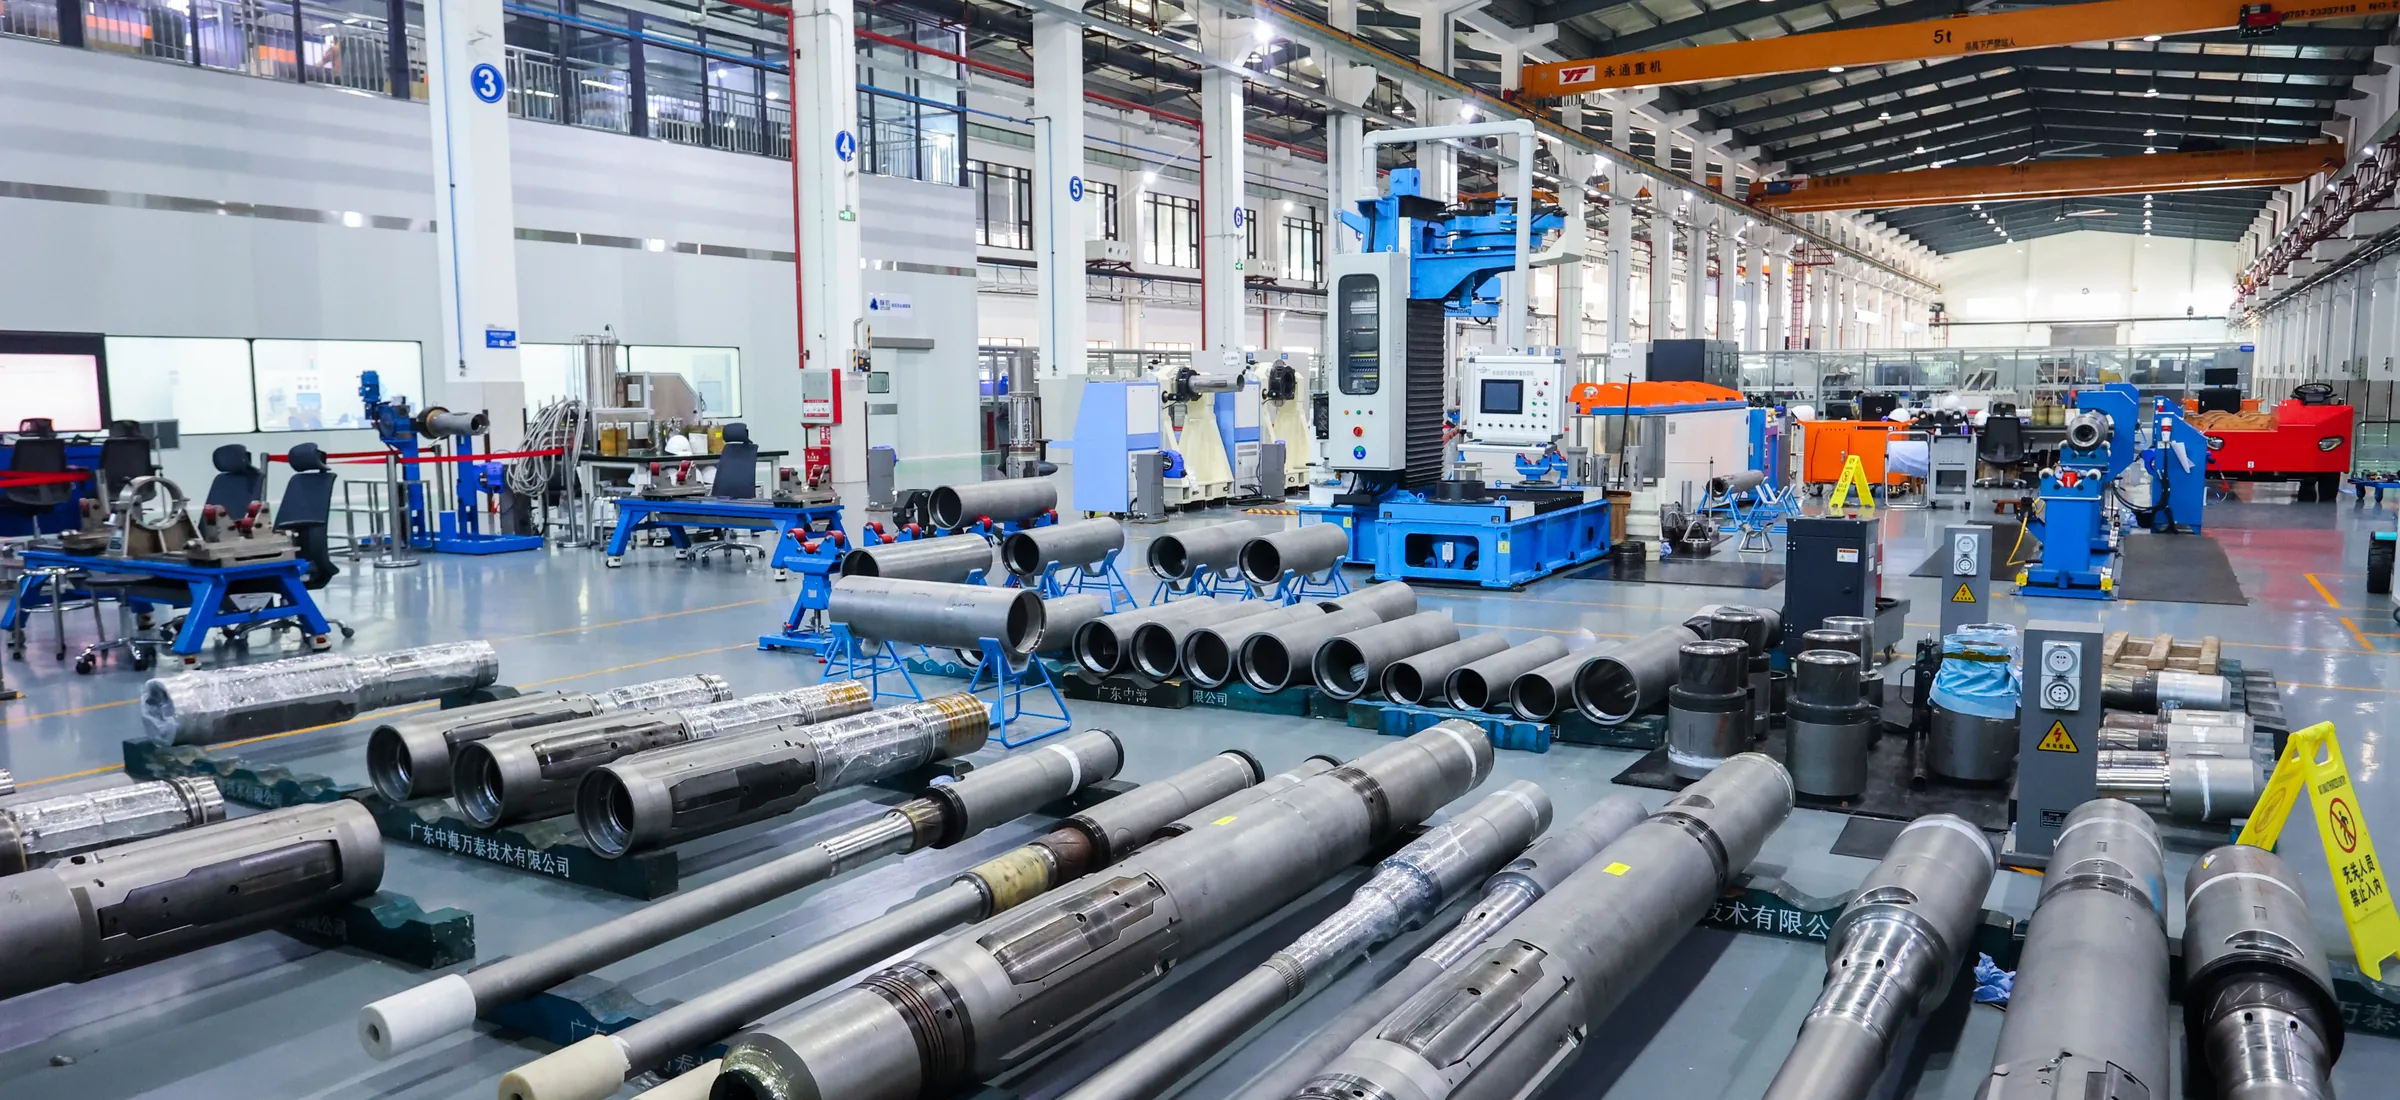
The structural parts — push blocks, ribs, housings and the drill collar family. Tell us which assembly your drawing belongs to and we will confirm the route.
Yes, in batch. P550 and 15-15-class non-magnetic steels are in routine production for drill collars and housings — both work-harden severely, and both are process problems we have solved rather than avoided.
NC38, NC46 and NC50 series. Send the drawing and we will confirm the connection type.
Material verification in-house, dimensional reports with every order, and — through our joint venture — high-temperature/high-pressure validation at 180 °C / 180 MPa on a Ø450 × 10,000 mm chamber.
No. We supply oilfield service and downhole tool manufacturers. The same process discipline is available to your program.
Upload your drawing via the RFQ form — an engineer replies within 24 hours with manufacturability feedback and a calculated quotation.
Related: Oil & Gas Industry|Deep Hole Drilling