Home/Capabilities/Gun Drilling

Gun Drilling Services

The smallest holes demand the deepest discipline.

Precision gun drilling from Ø2 to 40 mm, up to 6,000 mm deep — fuel-system bores, hydraulic galleries, sensor passages, and cooling channels where straightness and surface finish are functional requirements, not cosmetic ones. On a 7-axis CNC gun drill we designed and built ourselves.

Send the drawing — Ø, depth and straightness callout are all we need. NDA welcome.
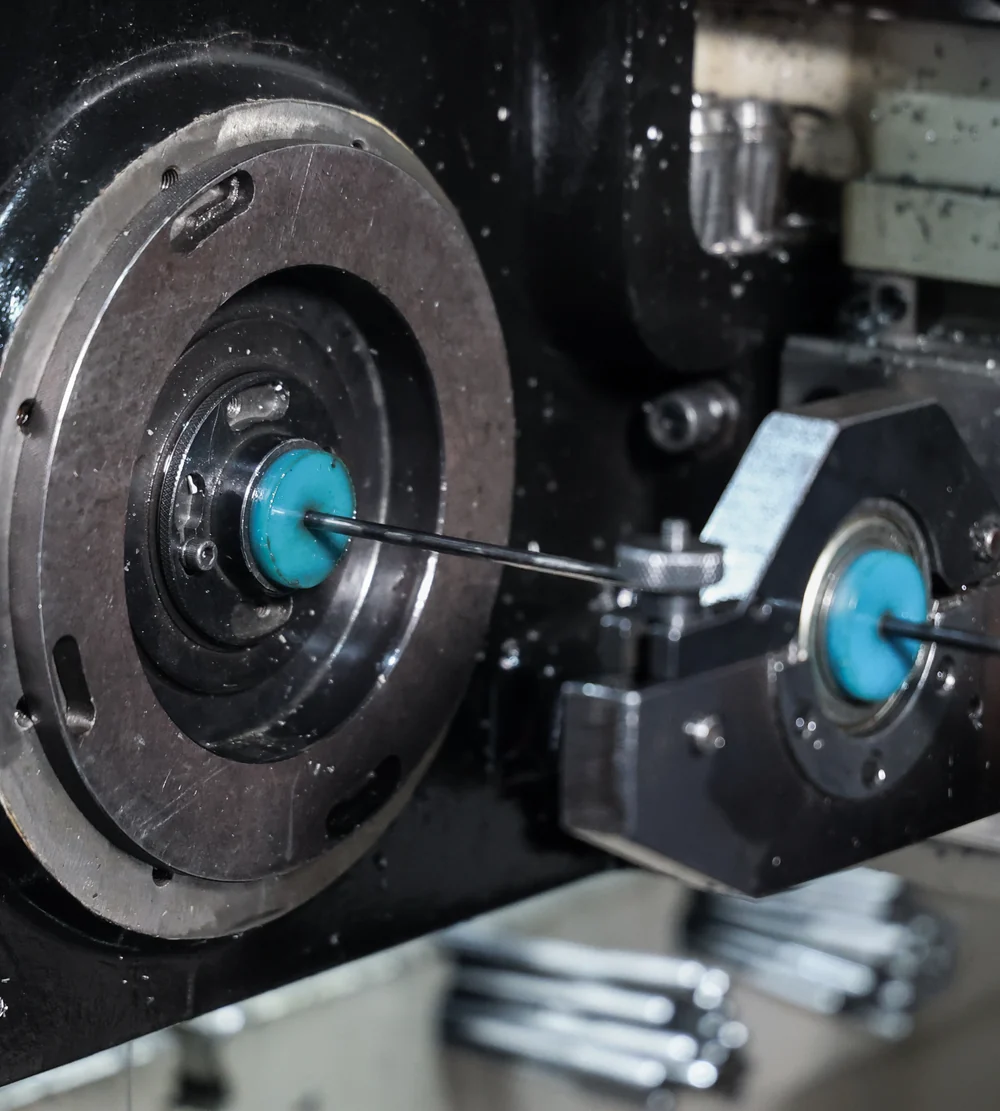
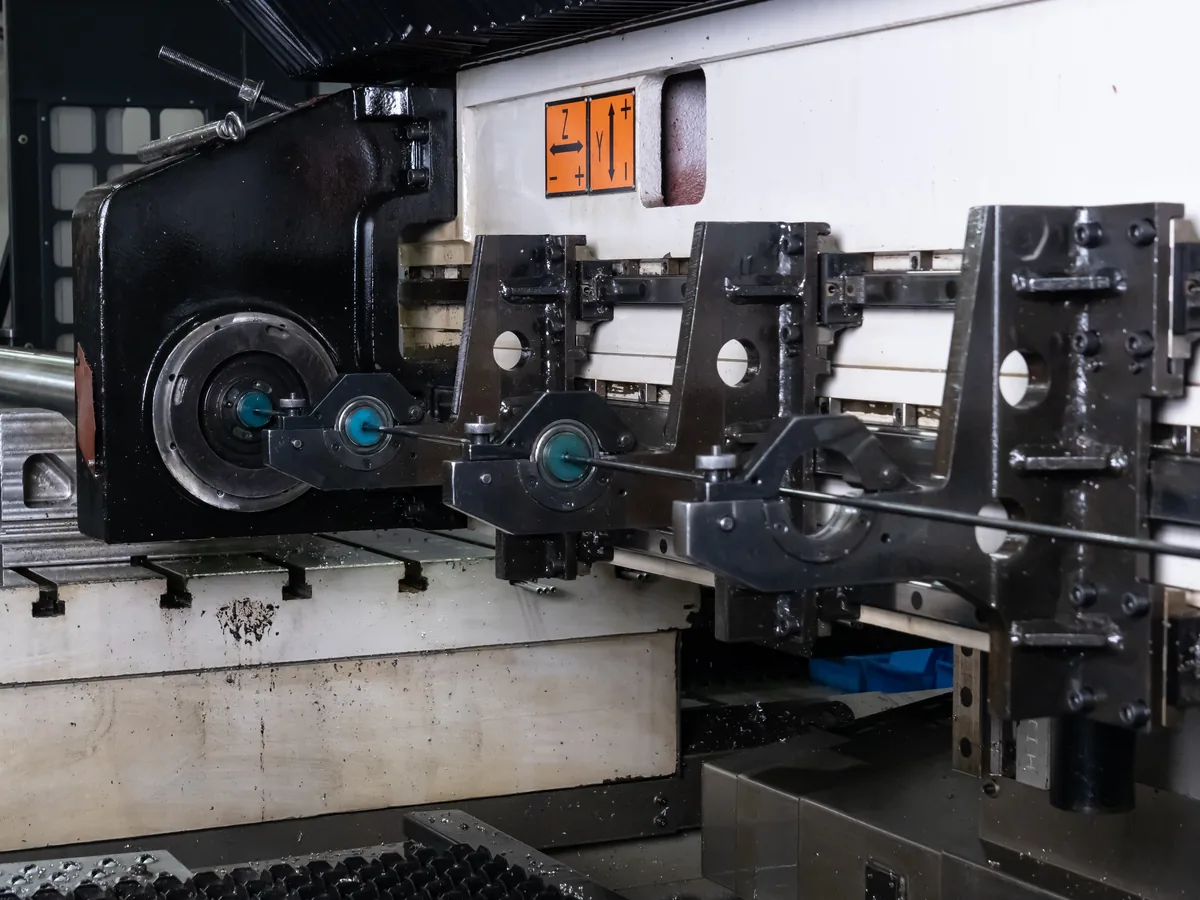
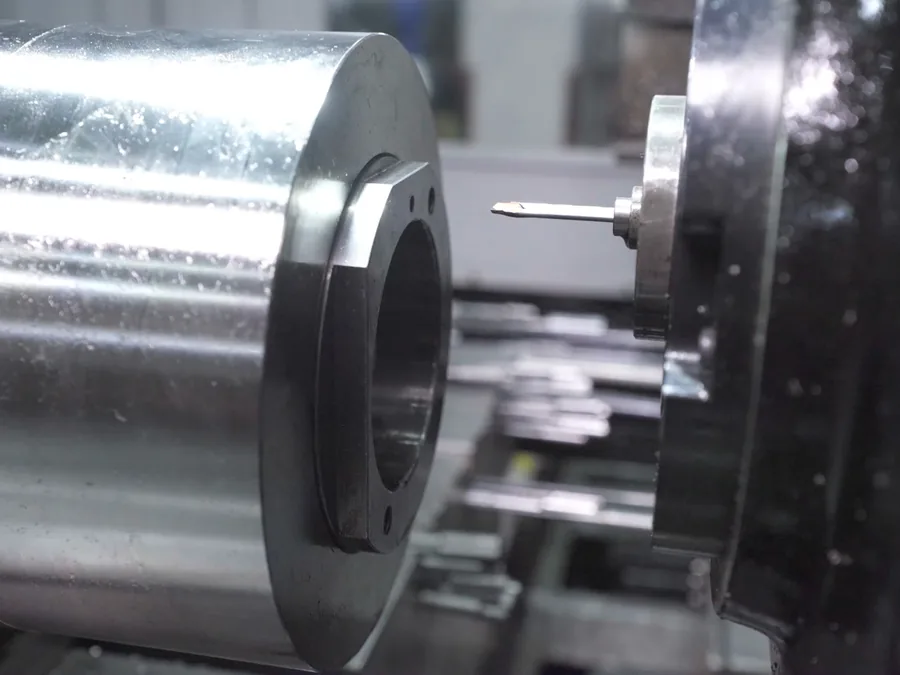
Gun drill passing through the drill bushing into the workpiece, high-pressure coolant at the cut
Ø2–40 mmTo 6,000 mm deepDrilled from both ends, 3 m strokes
Why small deep holes are their own discipline

Scale a hole down and the physics
does not scale with it.

Slender gun drill running through a line of guide bushings into the workpiece

Capability

ParameterCapability
Diameter rangeØ2 – 40 mm
Maximum depth6,000 mm (6 m) — drilled from both ends, meeting in the middle
Hole deviation≤ 0.8 mm over a 3,000 mm single-pass run
Depth-to-diameter ratioBeyond 600:1 in the Ø3–10 mm range — production work
MaterialsHigh-strength steels, stainless, superalloys (Inconel 718), titanium
Typical partsDrill collars, ACPR resistivity tools, common-rail pipes, hydraulic manifolds & galleries, mold cooling channels
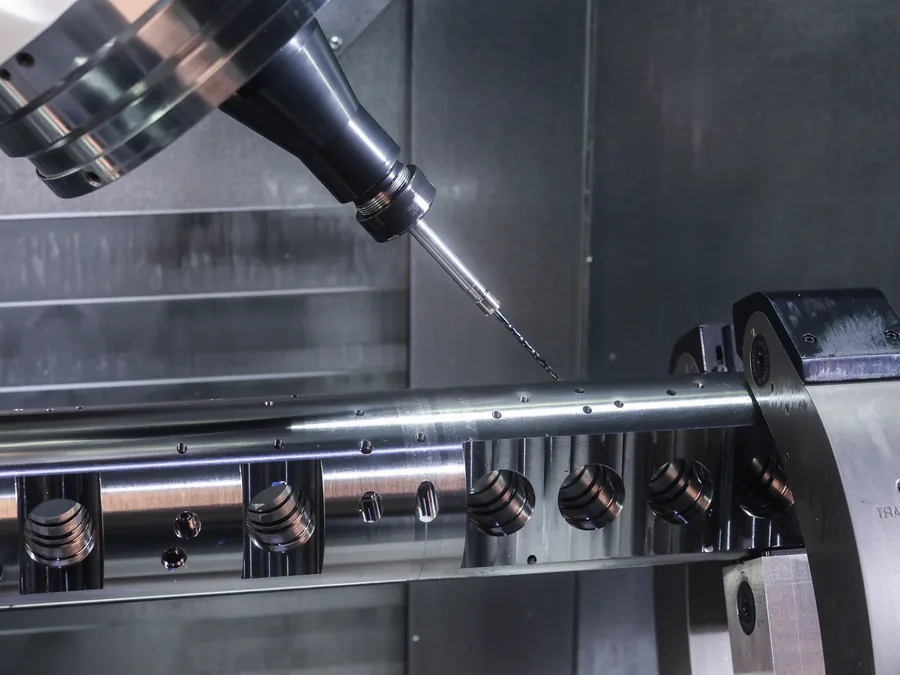
Angled / space gun drillingAntenna holes, sealing holes and galleries at compound angles — on the 7-axis machine, to the same depth discipline
Equipment13 gun drills, all designed and built in-house — deepest holes on the 7-axis FWZ-M2030B class

Proof, in numbers:

  • Ø5 mm × 1,800 mm — a gun-drilled bore that long, with a minimum wall of only 12 mm
  • 16 sealing holes at compound angles, in 8 groups — drilled in one setup on our 7-axis gun drill
Gun drill head and coolant supply at the cutting edge
Why we built our own gun drill

Gun drilling is where this company’s
machine-building story began — literally.

Machining centre in operation on the Zhongnan floor

Gun drilling is where this company’s machine-building story began — literally.

The common-rail unit program did not just need long holes; it needed precision holes in high-strength steels, at lengths no available machine could hold. When both the technology and the machines were closed to us, we built our own — and among them was a 7-axis CNC gun drill, 6-meter drilling depth, born from a part no one would teach us to make.

That origin still shows in how we run the process today: drill bushing wear is a monitored parameter, not a surprise; coolant chemistry is a controlled variable, not a consumable; and when a hole drifts, the people diagnosing it understand the machine down to its design intent — because they designed it.

Full machine-building story: Custom Machine Tools →

Where Our Gun Drilling Is Working

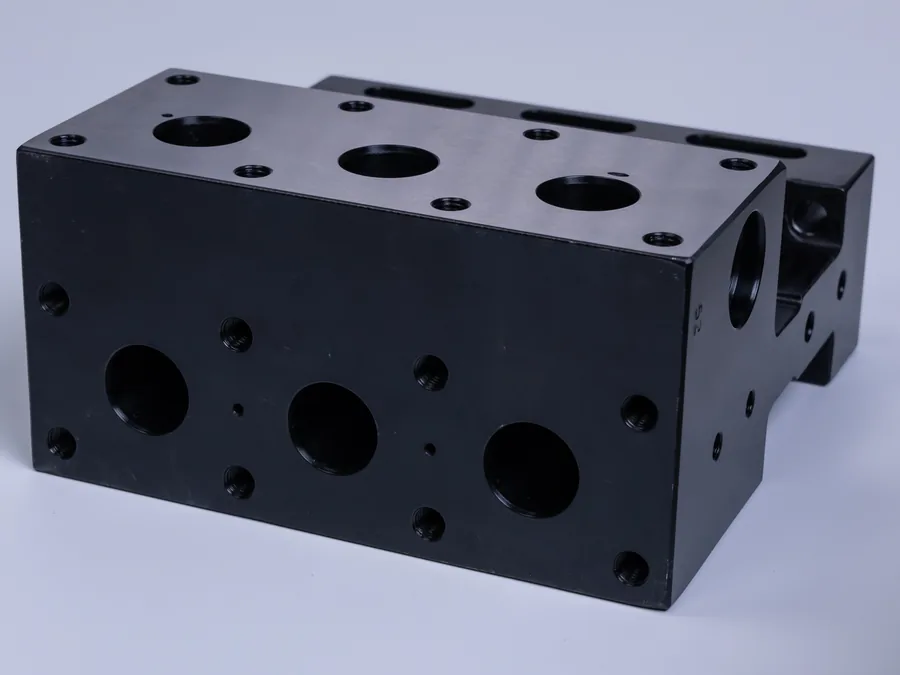
Angled and cross-hole machining for hydraulic galleries
Cross-hole and angled drilling — hydraulic galleries
Pump body — cross holes and bores finish-machined
Pump body — cross holes and bores, finish machined
Mold cooling channel component
Conformal cooling channel work
ApplicationWhy gun drillingOur record
Marine fuel systemsCommon-rail pipes — thousand-bar fatigue cycles demand functional bore finishBuilt when the technology and equipment could not be bought; certified by 7 classification societies; in service aboard China’s polar research vessel
Hydraulic manifoldsIntersecting galleries in valve & control bodiesIn production — hydraulic control unit bodies for downhole tools
Mold cooling channelsConformal cooling bores in large moldsOur company began as a tooling & mold shop in 1993 — cooling channels are in our DNA
Rotary-steerable drilling & logging systemsAntenna-hole passages in drill collarsIn production
FAQ

FAQ

Q: What depth-to-diameter ratio can you hold?

Extreme ratios are our daily work — beyond 600:1 in the Ø3–10 mm range, and depths to 6,000 mm at small diameters. The achievable ratio depends on diameter and material; send the drawing and we will tell you honestly what is achievable.

Q: What tolerance and straightness can you guarantee?

We do not quote numbers before seeing the print — diameter, depth, and material decide the answer. For reference: hole tolerance ±0.02 mm, bore finish Ra 1.6 μm, straightness 0.5 mm/m — and hole deviation within 0.8 mm over a 3,000 mm single-pass run. Our gun drill was built in-house for a thousand-bar fuel-system application; precision holes are where this machine came from.

Q: Can you drill intersecting or angled holes?

Cross-hole and gallery work is part of our hydraulic manifold production — angled holes run on the 7-axis CNC gun drill we built in-house, covering −90° to +90° with an angular tolerance of ±3′.

Q: Do you take small batches or single prototypes?

Yes — single-piece research and prototype work runs through our Custom Manufacturing line, built for research institutes. Batch fuel-system and hydraulic work runs on the production floor.

Q: Can you gun drill customer-supplied blanks?

Yes — full-service from our material, or your supplied blanks.

See all questions we get asked →

Send the Hole That’s Too Small, Too Deep — or Has to Be Dead Straight

Upload your drawing — fuel-system bore, manifold gallery, or cooling channel. Within 24 hours, an engineer responds with process feedback.

Related: Capabilities Hub|Deep-Hole Drilling (BTA)|Marine|Custom Machine Tools

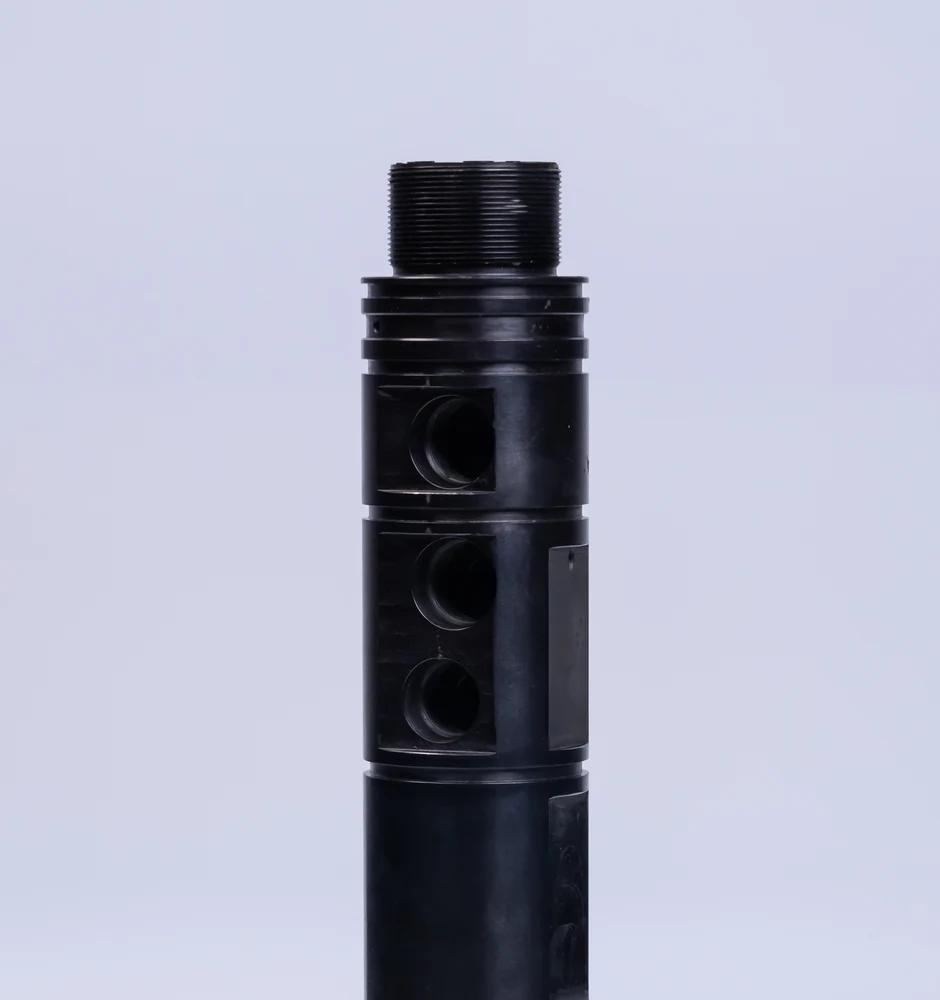
Gun-drilled injector body — threaded end and cross holes at compound angles
Injector body