Custom Machine Tools

We don’t just run machines. We build them.

When neither the technology nor the machines were for sale, we answered by building our own. A 6 m five-face gantry machining center, the 12 m FWB-L12010 floor-type boring and milling machine, an 8-meter CNC lathe, a 7-axis gun drill — and when production needs a machine the market does not offer, we build that too.

Send the drawing — if no machine on the market can make it, we will build one that can.
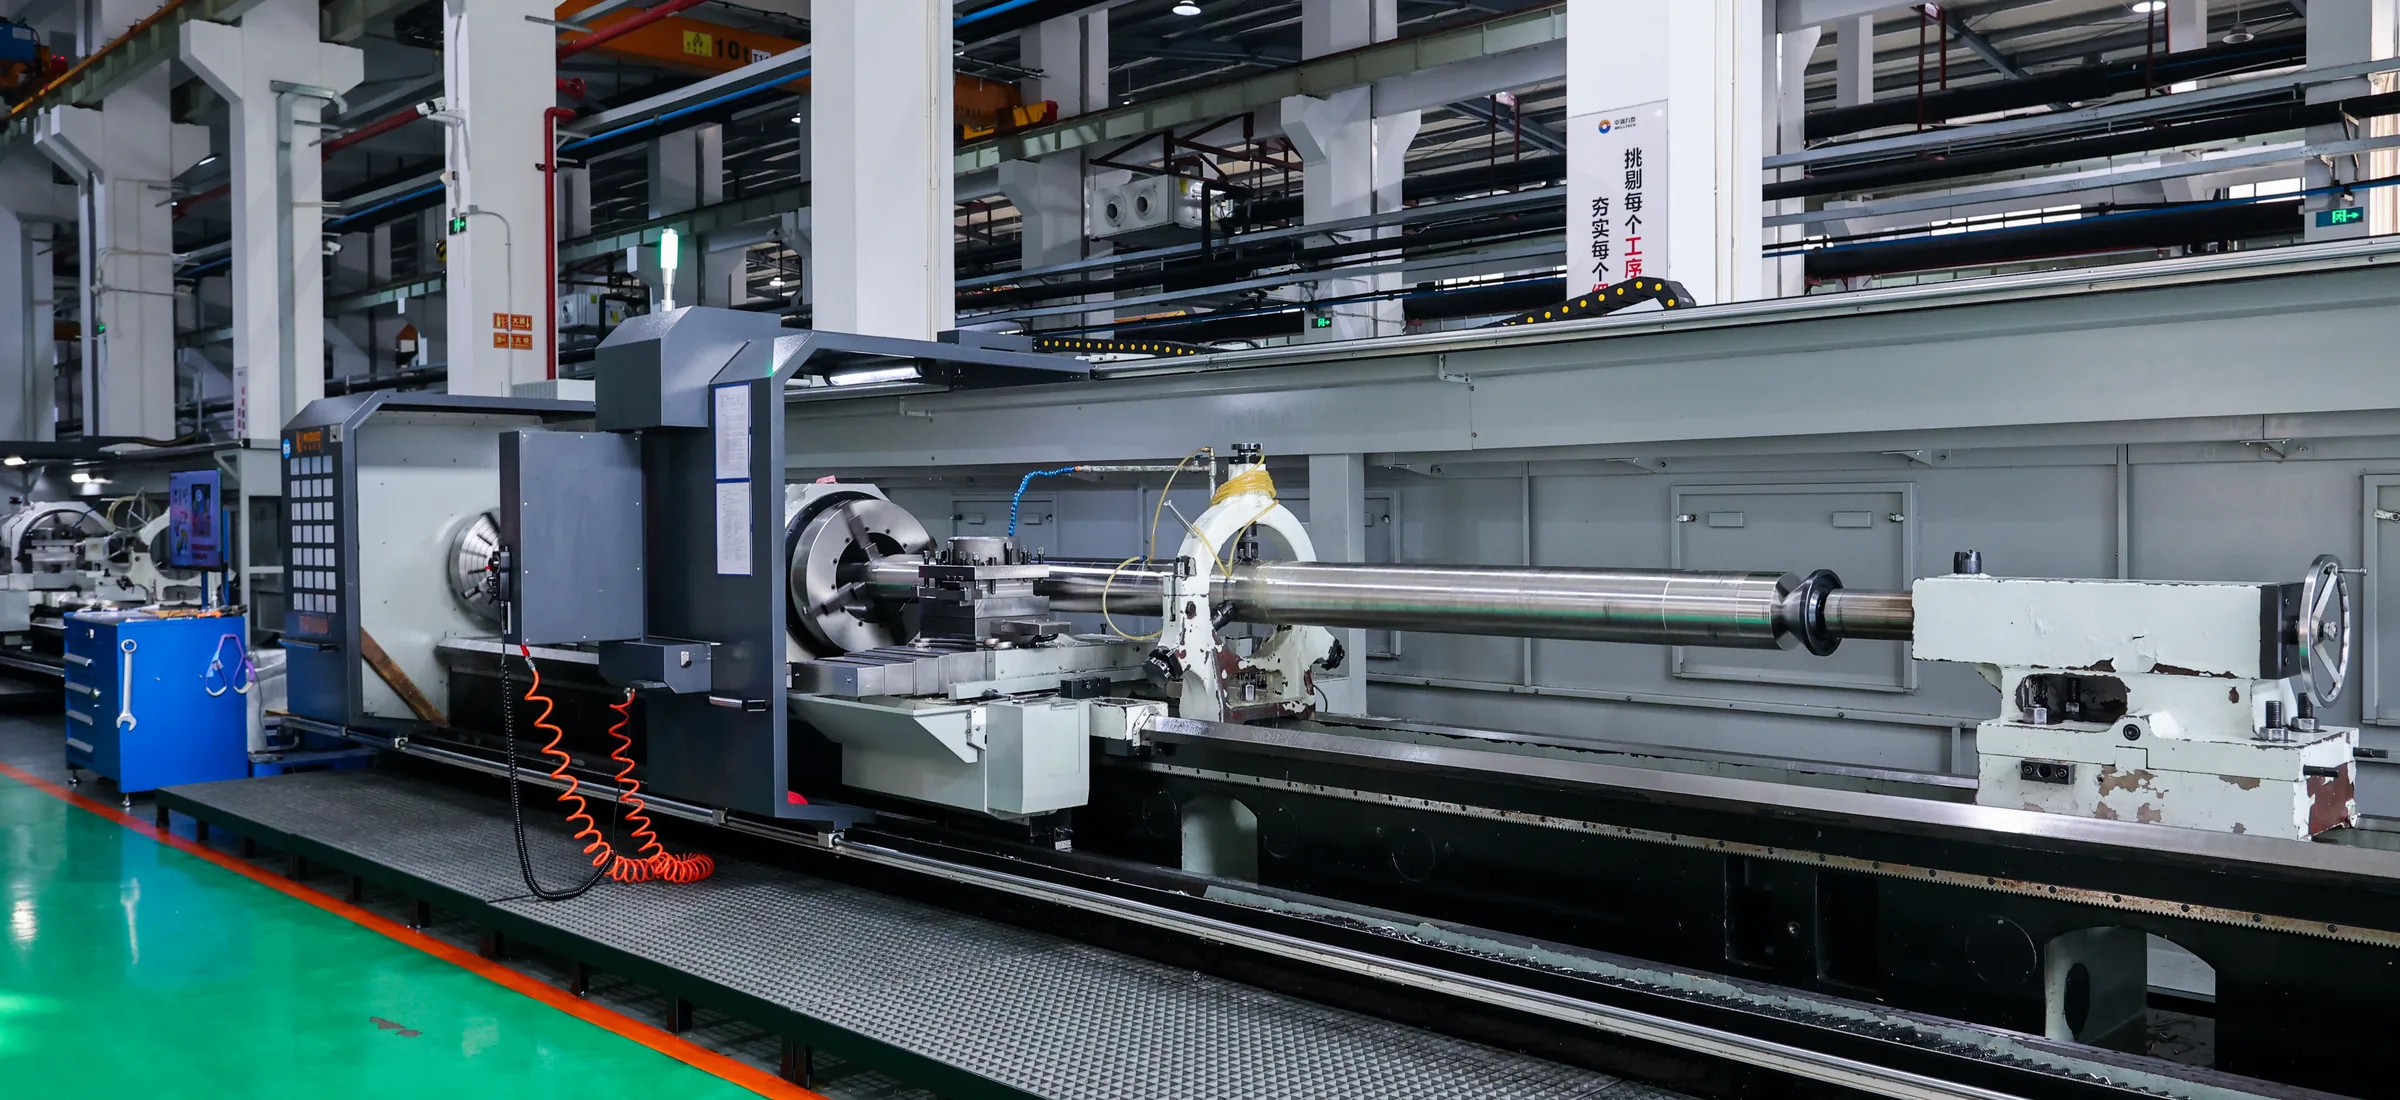
Self-built FWT-80800 eight-metre CNC lathe — chuck, steady rest and a long shaft in position
Built hereFWT-808008 m between centres, our own design

Why We Build Machines

In the early 2000s, large marine engine components — common-rail units, cylinder blocks, cylinder heads — were import-only, available from a handful of foreign suppliers. Neither the machining technology nor the machines were for sale.

Our founder’s account of that decision:

“We developed the FWG-M1260 gantry machining center, the 12-meter-travel FWB-L12010 floor-type boring and milling machine, an 8-meter CNC lathe, and a 7-axis 3-meter deep-hole CNC gun drill — solving the chokepoint machining problems of key engine components.”— Xu Guan, Founder

No machine on the market could make these parts. So we built the machine first — and the part followed. The common-rail unit followed — ten meters long, 1,050 bar working pressure — and with it, a machine-building capability that has never left the company.

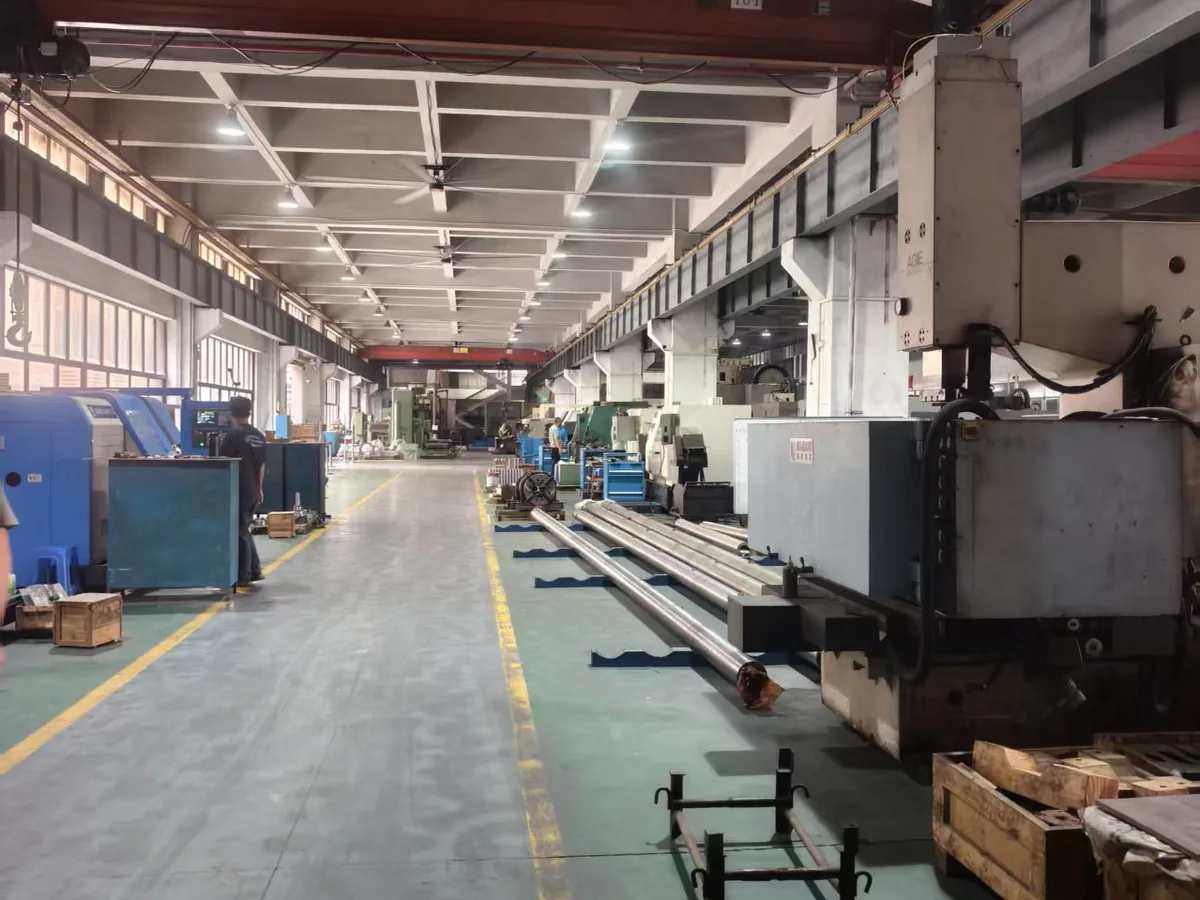
The original Zhongnan workshop — gantry crane, machine line along the aisle
1993The first workshopWhere the building started

The Machines We Built

Every machine on this table was designed backward from a part that existing machines could not hold. That is what “custom” means here: not a catalog with options, but a machine born from a process requirement. And where a market machine came close, we modified it — and armed it with tooling of our own design.

ModelTypeKey specificationsBuilt to solve
FWB-L12010CNC floor-type boring and milling machine — 4-axis simultaneous, four faces machined in one setupX travel 12,000 mm; Y travel 800 mm; Z travel 1,200 mmFuel common-rail units for large marine engines — the chokepoint part no market machine could hold at the time (see founder’s account in §2)
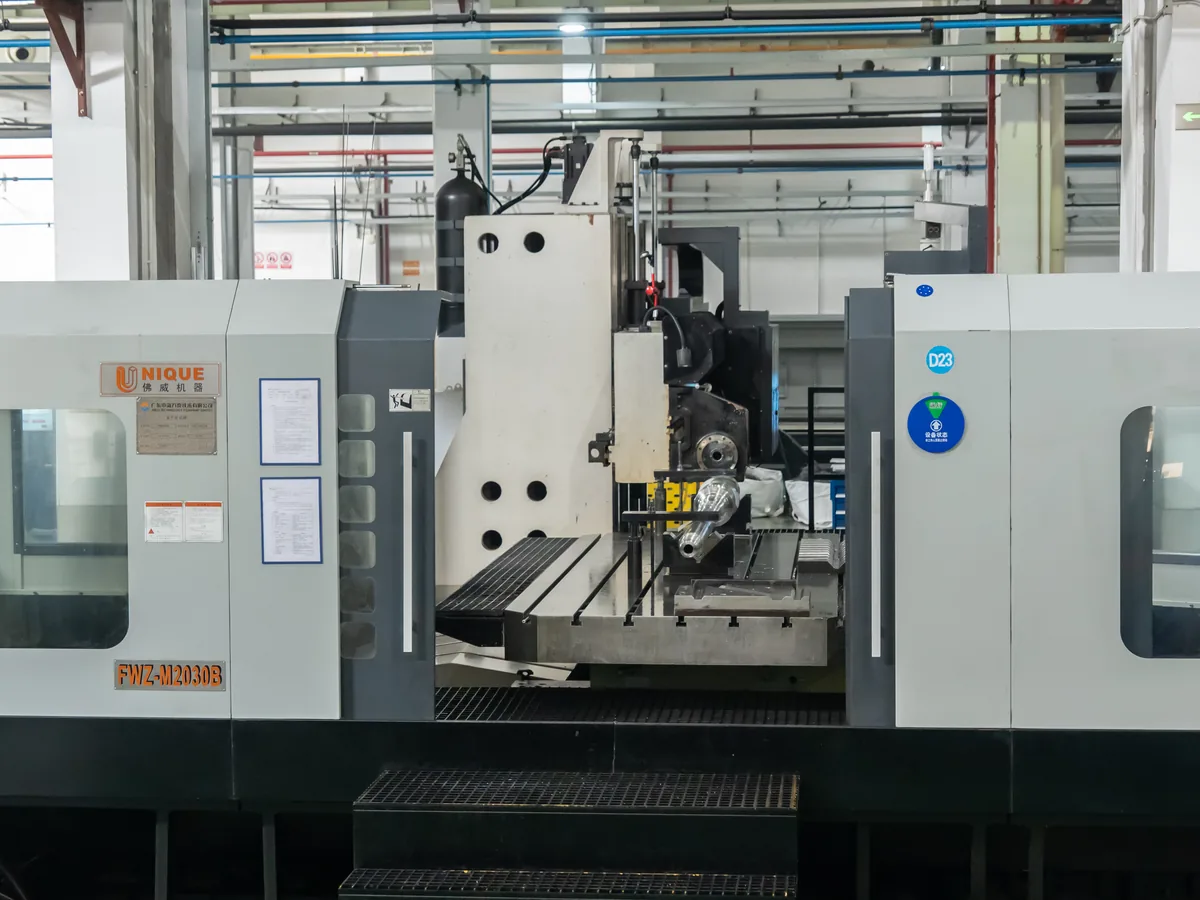
FWZ-M2030B7-axis CNC gun drill6,000 mm drilling depth; work zone 3,250 × 1,000 × 2,600 × 2,880 mm; BT40Precision deep holes: fuel-system bores, long shafts
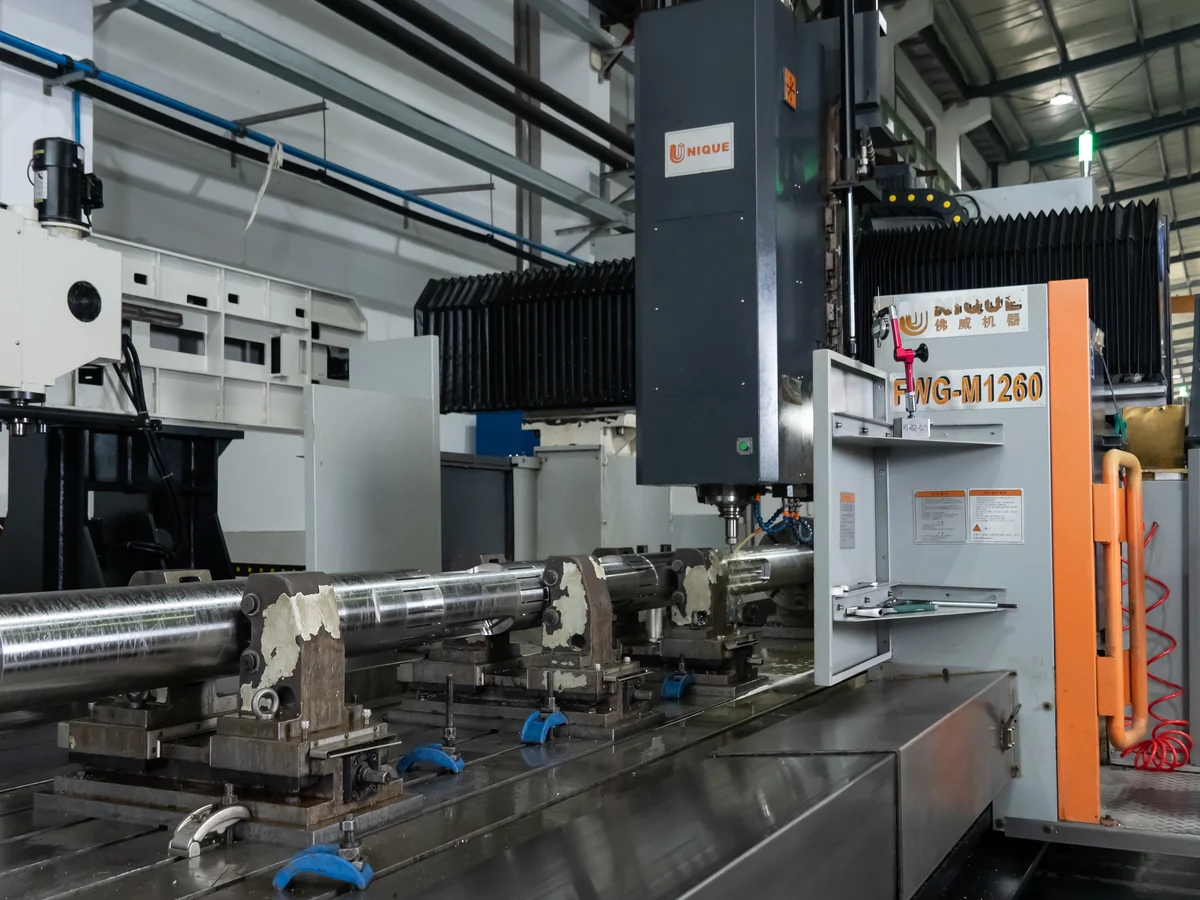
FWG-M1260Gantry machining centerTravels 6,000 × 1,200 × 650 mm; BT-50 spindle; 6,000 rpm; table load 10,000 kg; 4th-axis rotary table; 5-face machining in one setup; Mitsubishi CNCLarge plate & block milling
FWT-808008-meter CNC latheØ800 × 8,000 mm; 40–980 rpmLong shafts, marine & downhole rotating parts
FWDHH-M4080 / FWDHH-L4070Deep-hole EDM drilling machine500 × 350 × 800 mm / 450 × 320 × 800 mm; electrode load 400 kgDeep, small-diameter holes in hardened and difficult-to-machine alloys — where mechanical drilling reaches its limit
FWDHH-L2390Ram-type mirror-finish EDM2,300 × 900 × 600 mm; table 2,500 × 1,200 mmLarge mould & die work — mirror finishes on hardened steel
Modified deep-hole drilling machinesDeep-hole drilling & boring — base machines modified in-house, running special tooling we design and build ourselvesBase machines sourced from specialist builders, then modified in-house for complex and profiled bores; cutting tools designed and manufactured in-houseLarge complex bores: internal annular grooves, eccentric bores, multi-step seal bores

These are not prototypes. They are the machines our parts run on today — across the group’s manufacturing base, on the same floor and with the same people. The FW-series machines on this table are built by our machine-tool subsidiary — Fowei Precision Machinery (Foshan), a specialist custom CNC machine-tool builder since 2002.

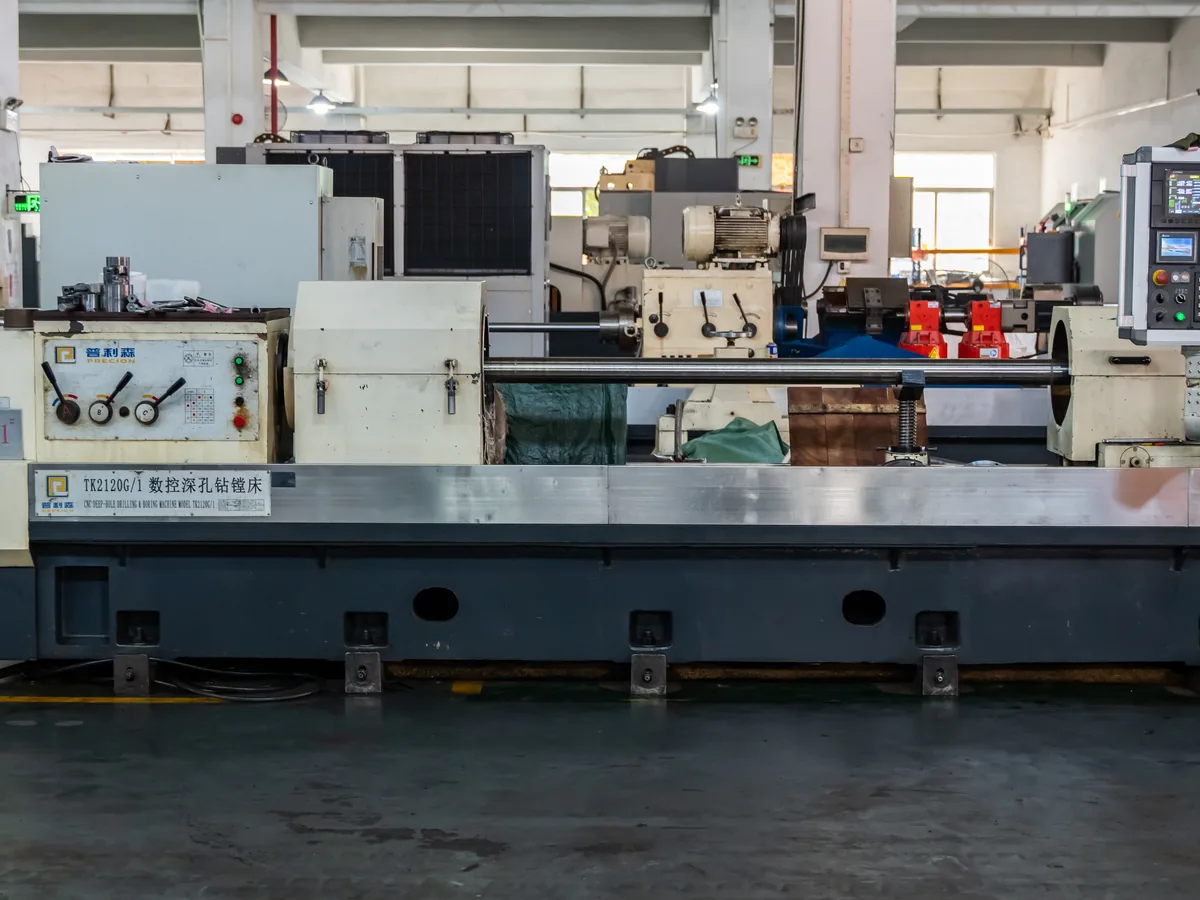
Twelve-metre deep-hole boring machine — long bed and machine head
12 m class deep-hole line
FWG-M1260 gantry machining centre — gantry head over a long shaft
FWG-M1260 gantry
Gun drilling machine — vertical body, control panel and drilling station
7-axis gun drill

What Building Machines Teaches a Machining Company

Here is the point our founder insists on — and the reason you will find no machines for sale on this site:

The machines were never the product. The machining is.

Building a machine teaches you what buying one never can:

So when your part runs on our floor, the people running it understand the equipment down to its design intent. A factory that can build its machine can hold its tolerance.

Flagship Case: The Machine and the Part

The problem. 2003: a major Chinese shipyard held the license for a top-tier marine common-rail diesel — and for two years, nobody in the country could machine its fuel unit. Ten meters of high-strength steel, rail bores holding 1,050 bar working pressure, tolerances that punished every micron of machine deflection.

The machine. With the process closed to us and the machines closed to us, we built the machines — including the FWZ-100200 deep-hole drill, drilling 10 m deep — and rebuilt the process alongside it: drill geometry, coolant strategy, bushing support, feed discipline.

The result. 2006: the first China-made marine common-rail units, ending the era when such parts could only be imported. Certification from seven classification societies followed; the units later entered service aboard China’s polar research vessel. And the machines stayed — still running, still teaching.

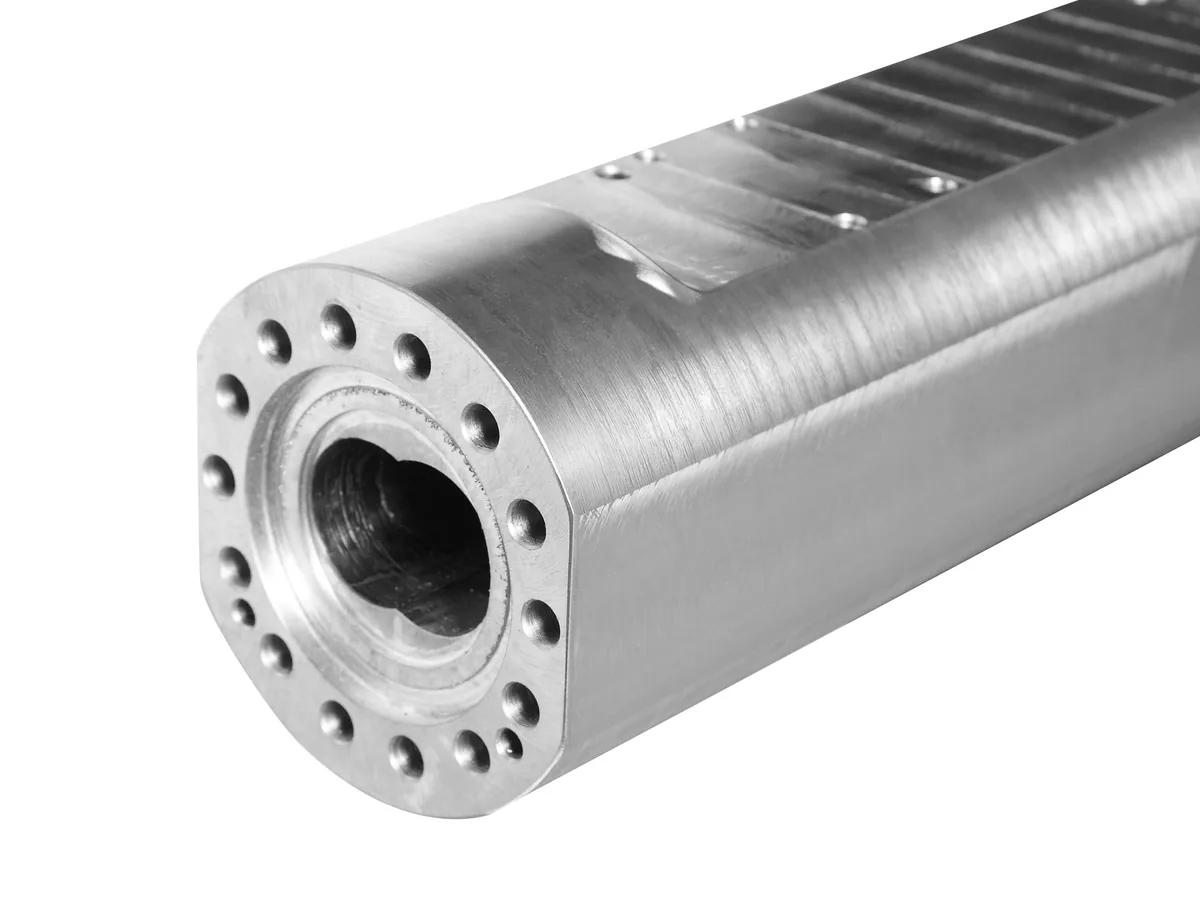
Common rail fuel pipe — flange face with bolt holes and the bore
2006Common rail fuel pipeThe part that started the machine building

Case 2 — the gun drill that holds its line

The problem. Ultra-long gun-drilled holes in large workpieces: beyond a certain length-to-diameter ratio, the drill’s own weight and the cutting forces walk the hole off line — and no stock machine offered the support strategy to prevent it.

The machine. The FWZ-M2030A CNC gun drill: a combined drilling-and-milling architecture with a long-nose BT40 spindle. A front steady rest pre-drills the guide bore; the spindle then retracts and the drill is carried by a tool cradle — an over-long drill, supported at both ends.

The result. Deep holes at extreme length-to-diameter ratios, held straight. The same support philosophy was later scaled into our 7-axis FWZ-M2030B class — 6,000 mm drilling depth.

More machine-building cases (process problem → machine solution → result) will be added as they are documented.

FAQ

Q: Do you sell machines?

No — the machines we build serve our own production lines. We do not take custom machine orders, domestic or overseas; machine building exists to serve our machining, not the other way around. What we do take: if you have a part no catalog machine seems able to hold — that is exactly the conversation worth having. We may already have built the machine for it.

Q: Can you modify or retrofit existing machines for a specific process?

For our own floor, yes — modifying and rebuilding machines for process requirements is part of how we work, and it is why our machining capability has no catalog ceiling. But it is not a service we offer: we do not take retrofit or machine-modification commissions.

Q: Why does this matter to me if I only need parts machined?

Because the machine is half the process. A supplier that built its equipment understands rigidity, thermal behavior, and wear from the inside — and when your part pushes a limit, that understanding is the difference between adjusting the machine and rejecting your drawing.

Q: What control systems do your machines run?

Mitsubishi, Siemens and FANUC — our gantry machining centers, 8-meter lathes and gun-drilling machines run Mitsubishi CNC; the deep-hole EDM machines run Taiwan-made controllers.

See all questions we get asked →

Run Your Part on Machines Their Operators Built

Upload your drawing. Within 24 hours, an engineer — who may well know the machine’s designer personally — responds with manufacturability feedback.

Related: Capabilities Hub|Deep-Hole Drilling|Gun Drilling|Our Story

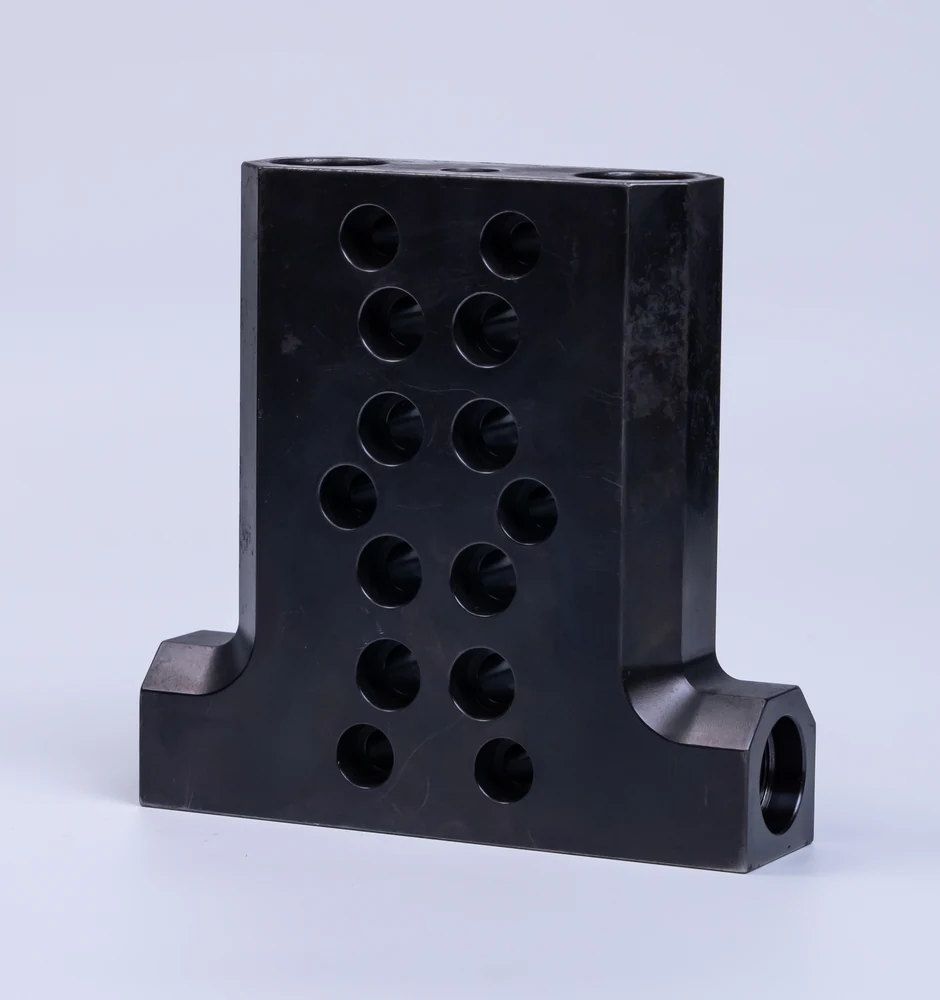
Pump cover — hole pattern and mounting feet
Pump cover