A metal part is not finished when the printer stops. That is where our part begins.
Metal additive manufacturing in stainless and tool steels, titanium, nickel superalloys, and cobalt-chrome — with the finish machining, heat treatment, coating, and inspection all in-house. We co-developed one of China’s first industrial metal 3D printers. Today the capability is ready for your program.

Additive manufacturing solved geometry. It did not solve surfaces:
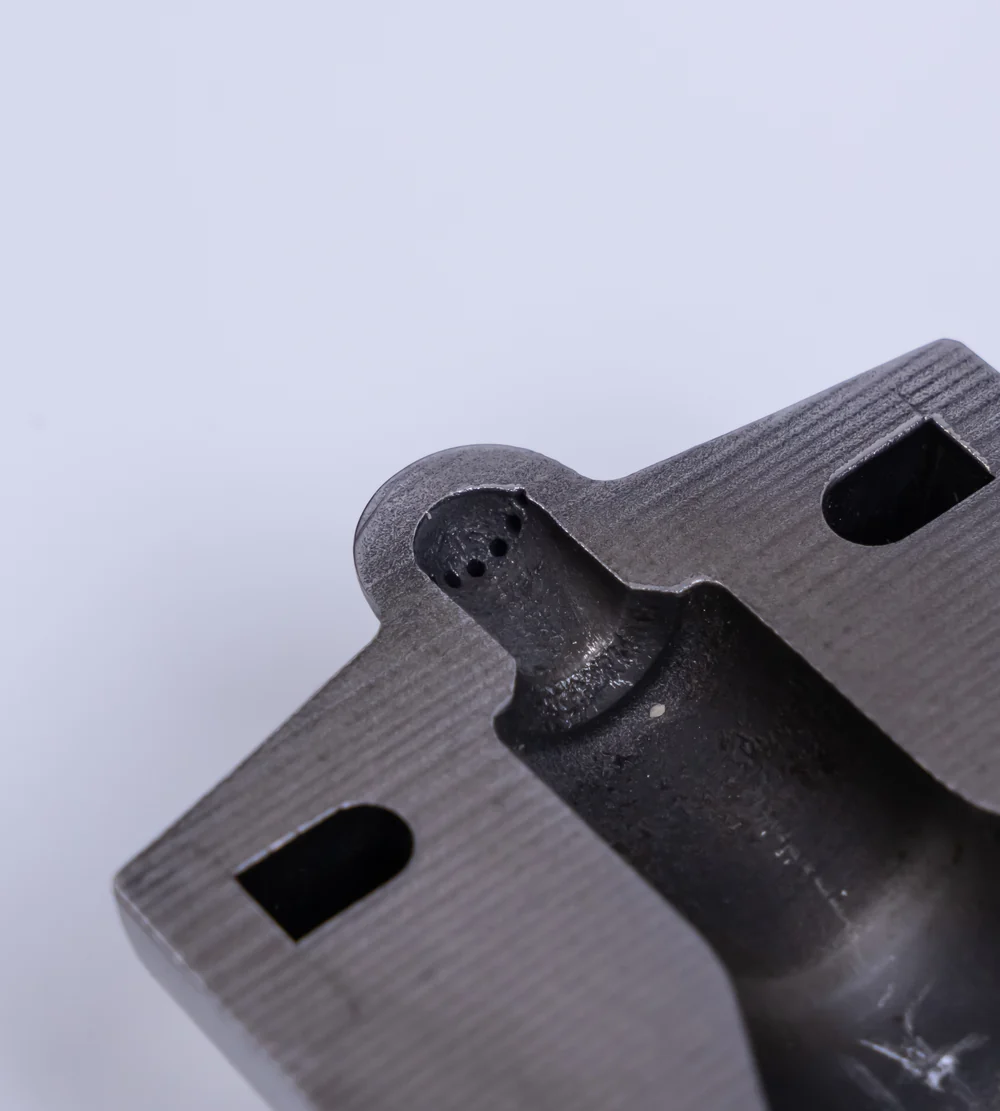
As-built roughness is an order of magnitude off precision requirements; sealing faces, bearing seats, and thread fits must be machined after printing
Residual stress from the build must be relieved before the part can hold its geometry; support removal and stress relief are process steps, not cleanup
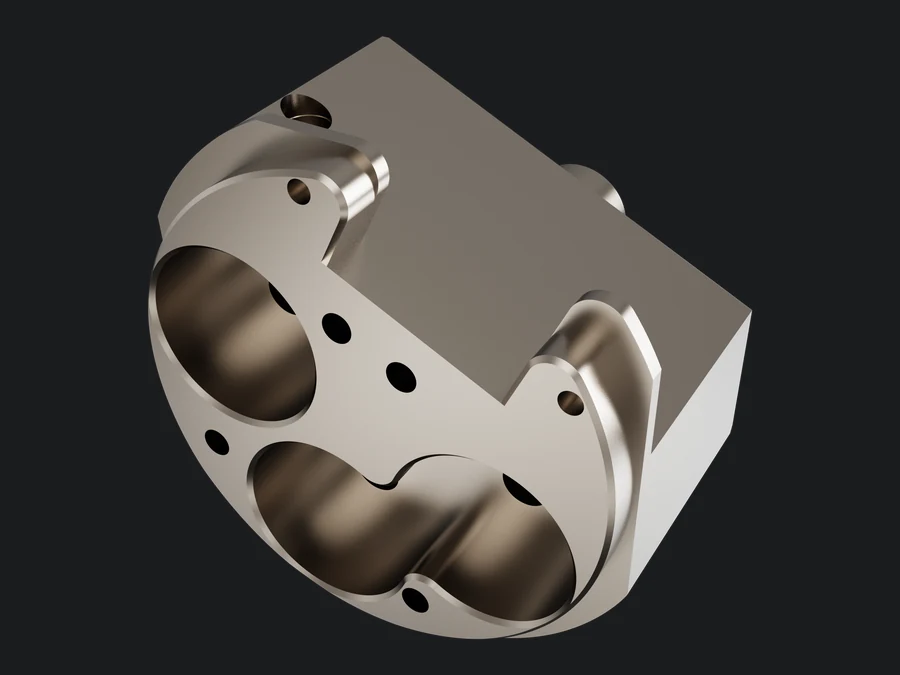
The interface surfaces, the bores, the threads: wherever the printed part meets the rest of the machine, precision machining takes over
Send a printed part out for machining and you inherit the classic dispute: the printer blames the machinist for scrapping the print, the machinist blames the printer for the distortion. Your project pays for the argument
We run both halves under one roof — the people who print your part and the people who finish it read the same drawing in the same building.

| Dimension | Capability |
|---|---|
| Materials | Stainless & tool steels · titanium alloys · nickel superalloys · cobalt-chrome |
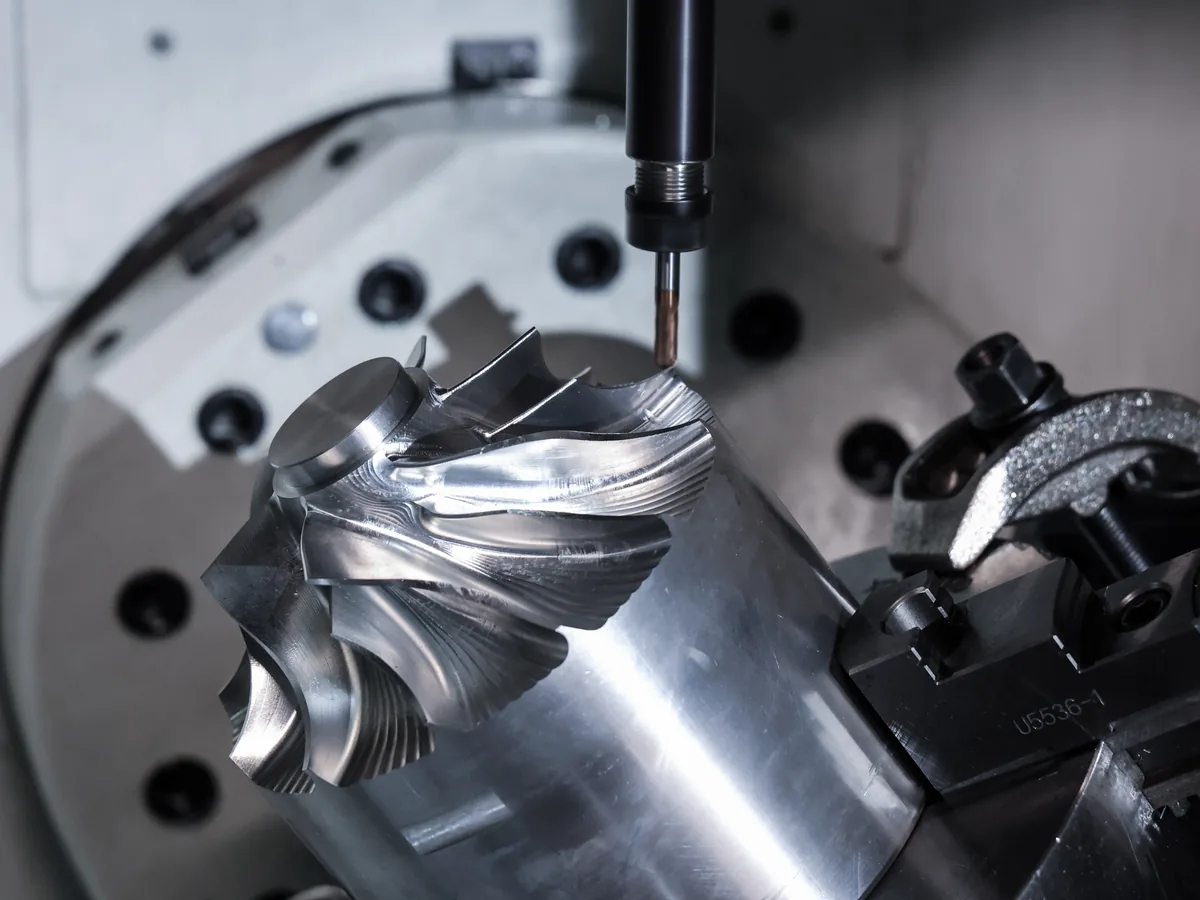
| Post-processing | Full in-house chain: 5-axis finish machining, precision grinding to Ra 0.1 μm, heat treatment, coating & plating |
| Typical work | Research prototypes, single-piece custom parts, complex geometries that machining alone cannot reach |
| Documentation | Material certificates and dimensional reports available per part |

In 2013 — when metal additive manufacturing was still a laboratory subject in most of the world — Zhongnan co-developed one of China’s first industrial metal 3D printers with South China University of Technology, as a major science and technology project of Foshan.
We did it for the same reason we build our own machine tools: when a capability our parts need does not exist, we create it. The printer was built to serve machining — and a decade later, that is still how we run it: additive where additive wins, machining where precision lives, one roof over both.
Single pieces and pilot parts with full documentation. Our rapid-prototyping line was built for you → Custom Manufacturing →
Send the drawing, and we will tell you honestly which features should be printed and which should be machined.
That sentence is the reason this page exists.
Stainless & tool steels, titanium alloys, nickel superalloys, and cobalt-chrome — with finish machining in the same alloys, in-house.
400 × 400 × 400 mm build envelope. For larger parts, hybrid strategies apply — printed sections finish-machined and integrated with machined components.
Yes — that is the point of this page. Critical features are finish-machined to your drawing, to 0.005 mm class tolerances and Ra 0.4 μm finishes where required, verified by our in-house metrology.
Our additive capability serves research, prototype, and single-piece work; for volume programs we will tell you honestly whether printing, machining, or a hybrid route is the right answer.
STL files, or 3D models from any major CAD software — attach them to the RFQ form (NDA first if you prefer).
Send your drawing — we will route each feature to the process that serves it best, under one roof. Within 24 hours, an engineer responds with process feedback.
Related: Capabilities Hub|Custom Manufacturing|5-Axis Machining|Custom Machine Tools